EN

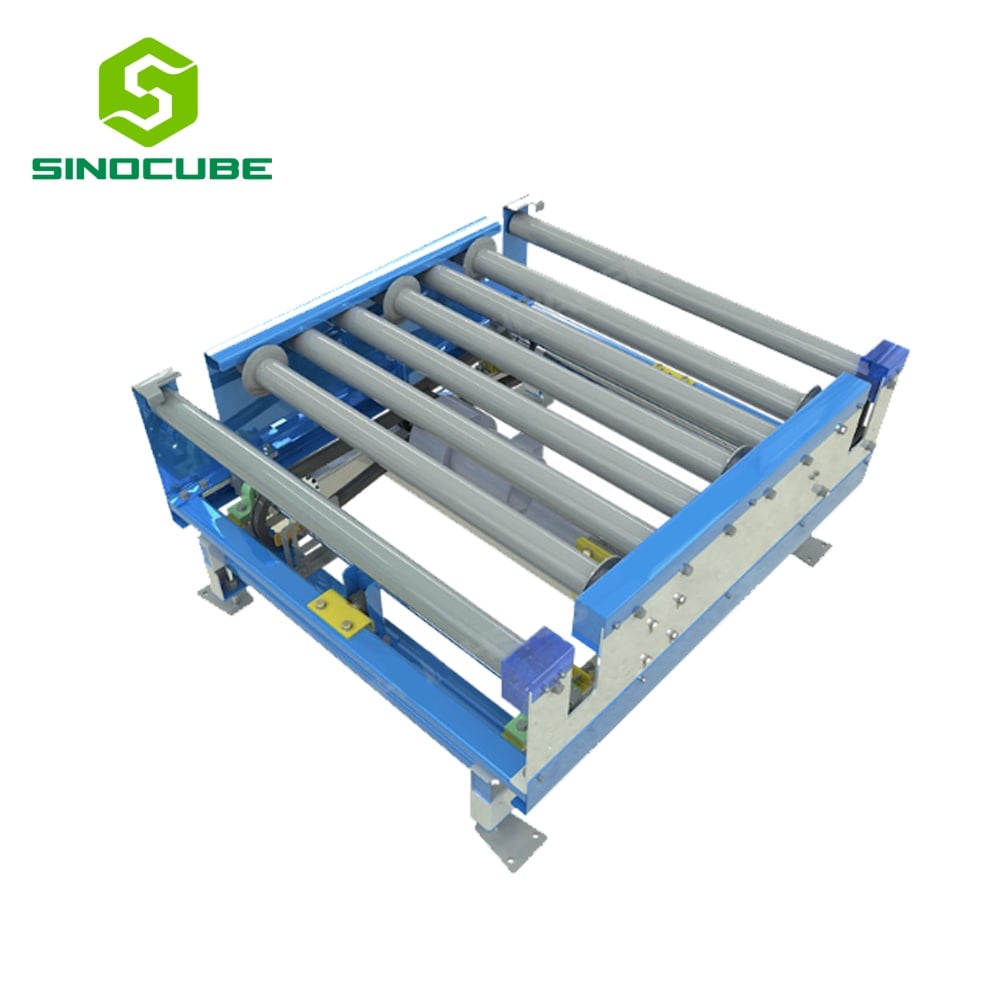
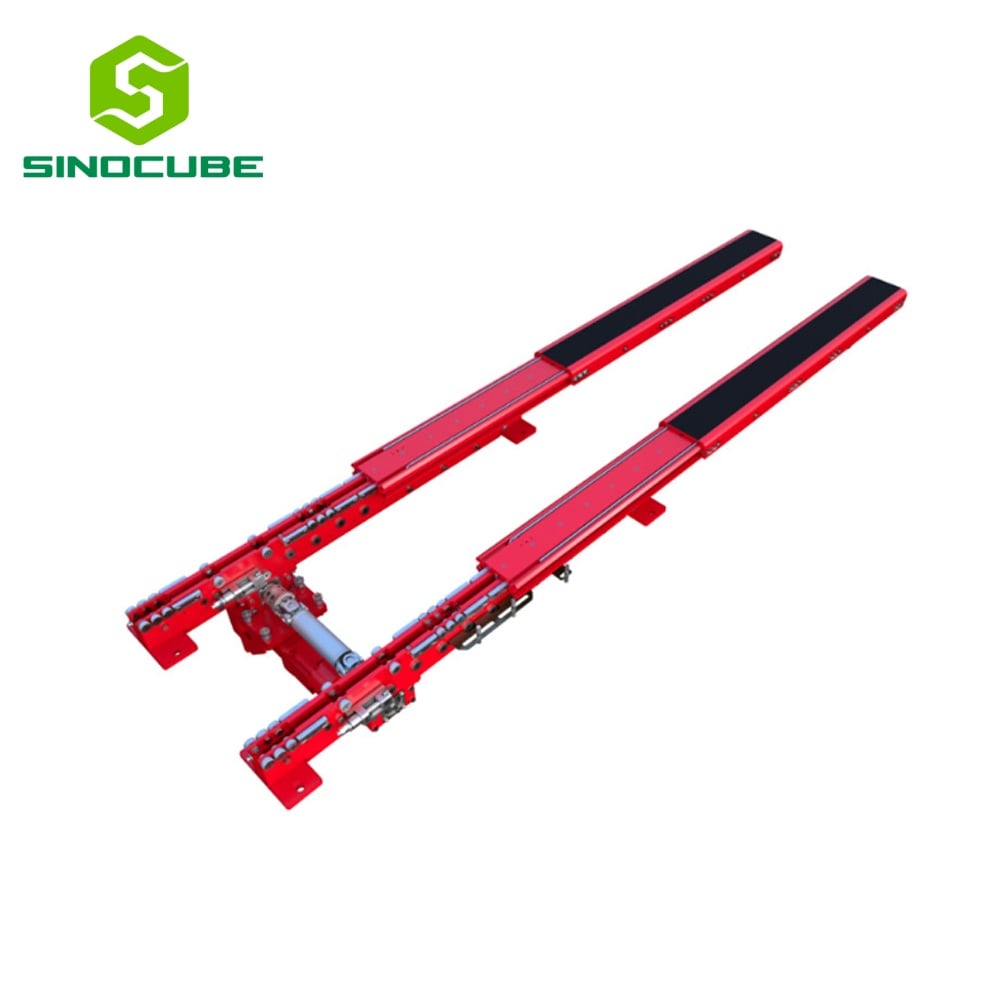
Lifting Transfer Unit Programmable Pallet/Box Handling System Anti-static Steel Rollers for Intelligent Warehouse
|
Place of Origin: |
China |
|
Brand Name: |
Sinocube |
|
Model Number: |
Lift Transfer Unit |
|
Certification: |
RoHS |
- Overview
- Recommended Products
Description:
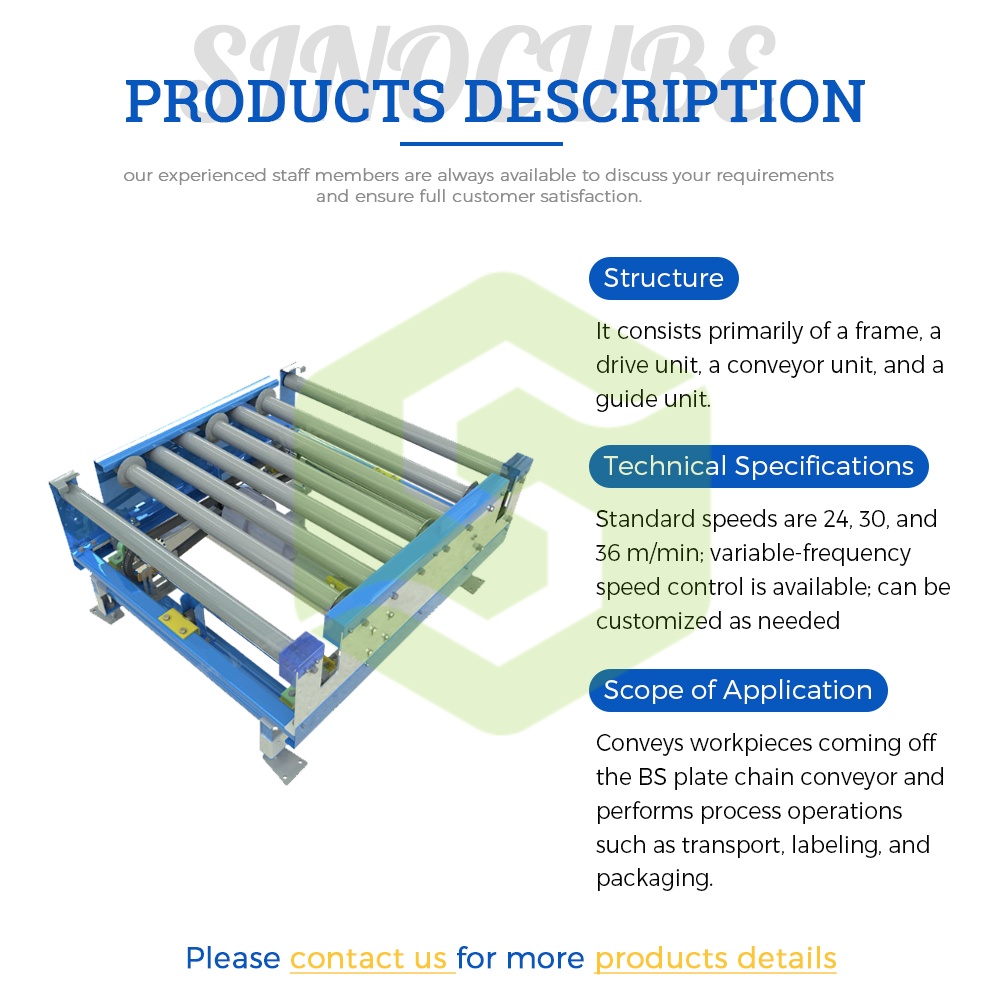
The Pallet Lift Transfer Unit is a versatile material handling device designed for the efficient transport and redirection of palletized loads, cases, and containerized goods within automated logistics and production systems. This unit serves as a critical junction in conveyor networks, enabling smooth directional changes, elevation adjustments, and seamless integration between different conveyor lines.
The unit consists of three primary assemblies: a high-strength aluminum alloy frame with adjustable support legs for precise height positioning; a robust drive system comprising a gearmotor, drive pulleys, and tensioning mechanisms with SKF bearings for reliable power transmission; and a transport assembly featuring conveyor rollers driven by belt loops. Side guide rails ensure accurate product alignment during transfer.
Engineered for heavy-duty applications, the unit handles substantial single-piece loads and withstands significant impact forces. It accommodates a wide range of materials—from boxes and bags to pallets and containers—with irregular or loose items transported on pallets or within totes. Standard operating speeds range from 24, 30, to 36 m/min, with variable frequency drive options available for customized speed control. Multiple units can be interconnected with other conveyors and specialized equipment to form complex, multi-functional logistics systems
Applications:
Manufacturing & Assembly Lines: Transfers pallets and workpieces between different process stages, feeding components to assembly stations, packaging lines, and labeling stations.
Warehousing & Distribution Centers: Enables efficient pallet routing between storage areas, sorting systems, and shipping docks within high-volume logistics operations.
Automotive Industry: Handles heavy automotive components and assemblies between production stages, supporting just-in-time manufacturing workflows.
Food & Beverage: Transports palletized goods through processing, inspection, and packaging stages in food production facilities.
E-commerce Fulfillment: Facilitates high-speed sorting and routing of palletized orders within fulfillment centers.
Cross-Docking Operations: Enables efficient transfer of goods between incoming and outgoing conveyor lines with minimal handling.
Palletizing & Depalletizing Systems: Works in conjunction with robotic palletizers to feed and remove pallets from automated stations.
Multi-Level Conveyor Networks: Interconnects conveyors at different elevations and orientations, creating compact, space-efficient system layouts.
Cold Storage & Freezer Environments: Reliable operation in temperature-controlled warehouses with optional hydraulic drive systems for extreme conditions.
Pharmaceutical & Cleanroom Applications: Suitable for handling palletized medical supplies and pharmaceutical products in controlled environments.
Specifications:
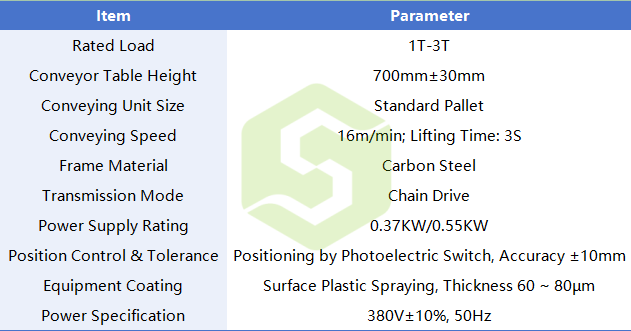
Competitive Advantage:
High-Efficiency Transfer: Ensures reliable, high-speed pallet and load transfer, significantly improving overall material flow throughput.
Heavy-Duty Load Capacity: Built to handle substantial single-piece weights and withstand high impact loads, suitable for demanding industrial applications.
Modular & Serviceable Design: Features a modular construction that simplifies assembly, disassembly, and maintenance, reducing downtime.
Flexible Speed Control: Standard speeds of 24, 30, and 36 m/min with optional variable frequency drive for customized operation.
Precision Load Guidance: Integrated side guide rails ensure accurate product alignment and smooth transitions between conveyor lines.
Stable & Reliable Operation: Simple mechanical design with minimal moving parts ensures high reliability and low maintenance requirements.
Accumulation Capability: Can be equipped with accumulation rollers to enable buffered, queue-style material flow.
Seamless System Integration: Easily connects with multiple roller conveyors and specialized equipment to form complex, multi-functional logistics systems.
Durable Construction: High-strength aluminum alloy frame with SKF bearings ensures long service life and consistent performance.
Energy Efficient: Optimized drive system reduces power consumption while maintaining high output.
Real-Time Monitoring: Integrated electronic control system continuously monitors operation, enhancing overall equipment stability and reliability.