Bulk Pallets: Heavy-Duty Storage Solutions

Contact me immediately if you encounter problems!

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

bulk pallets

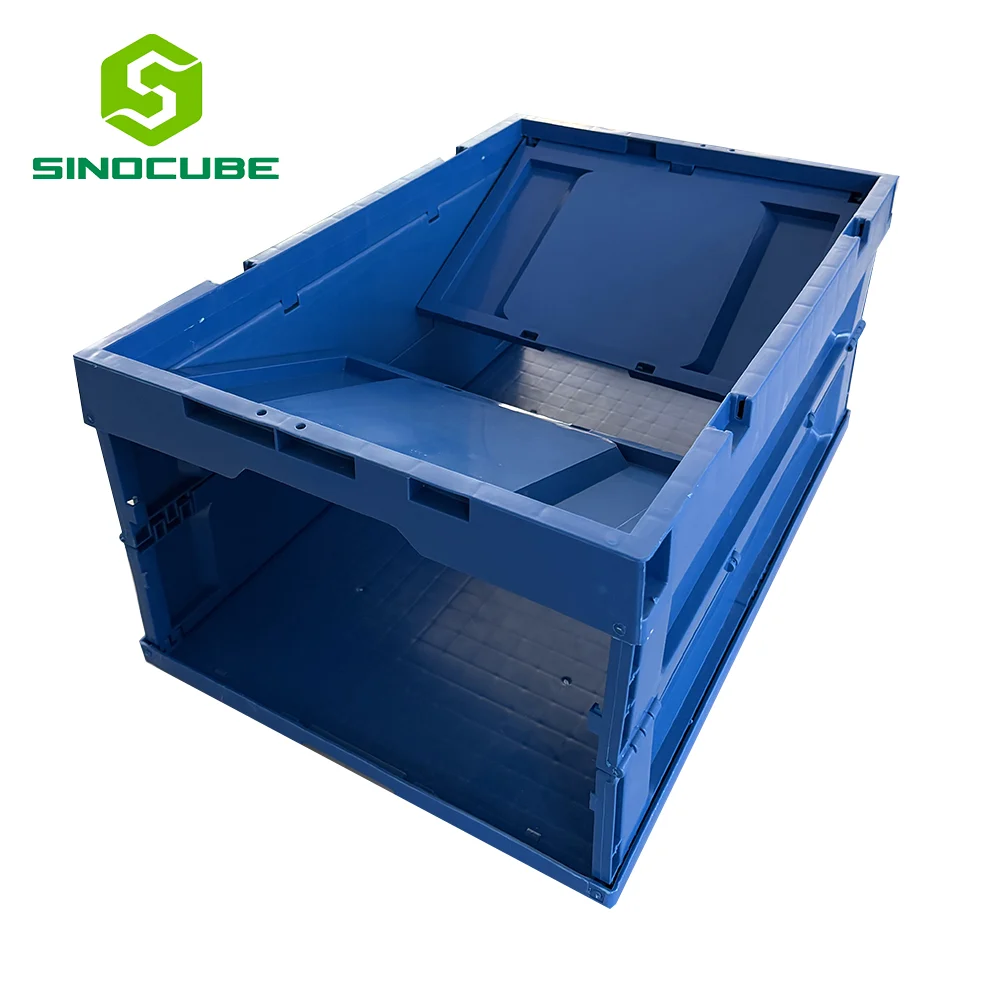
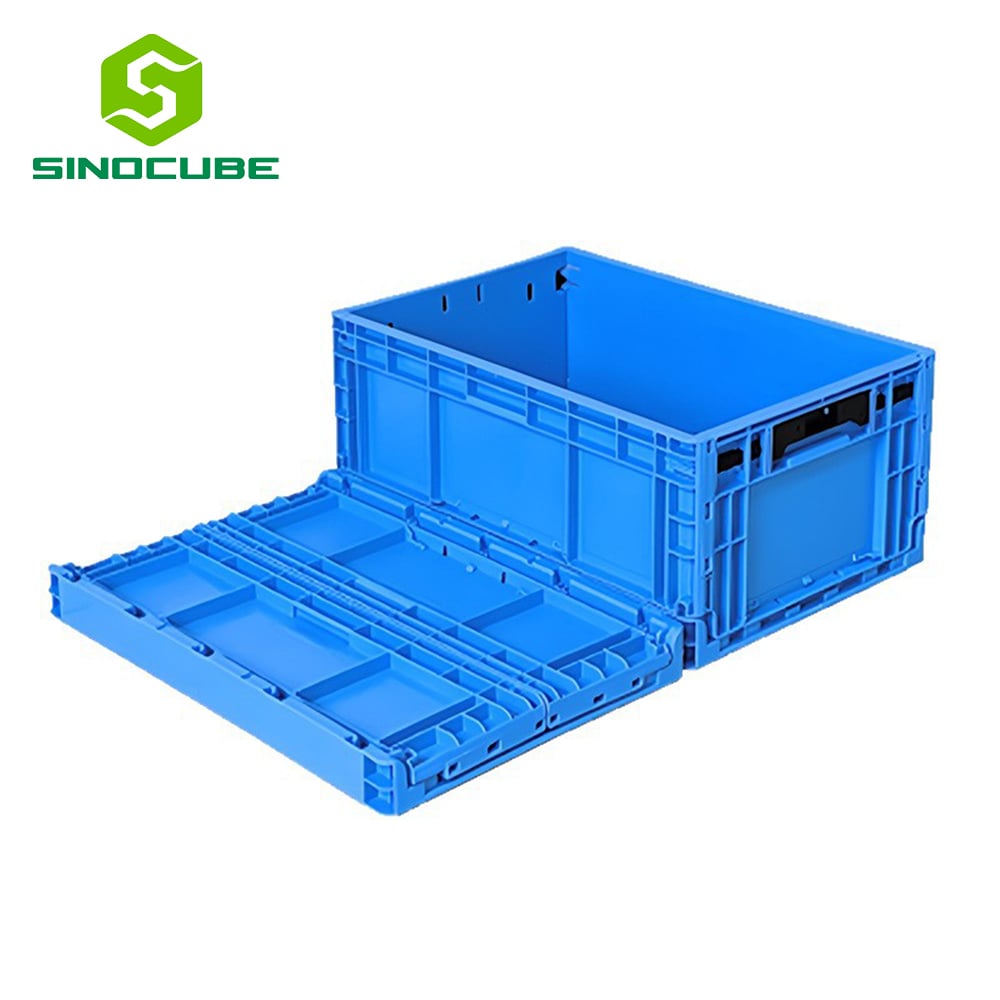
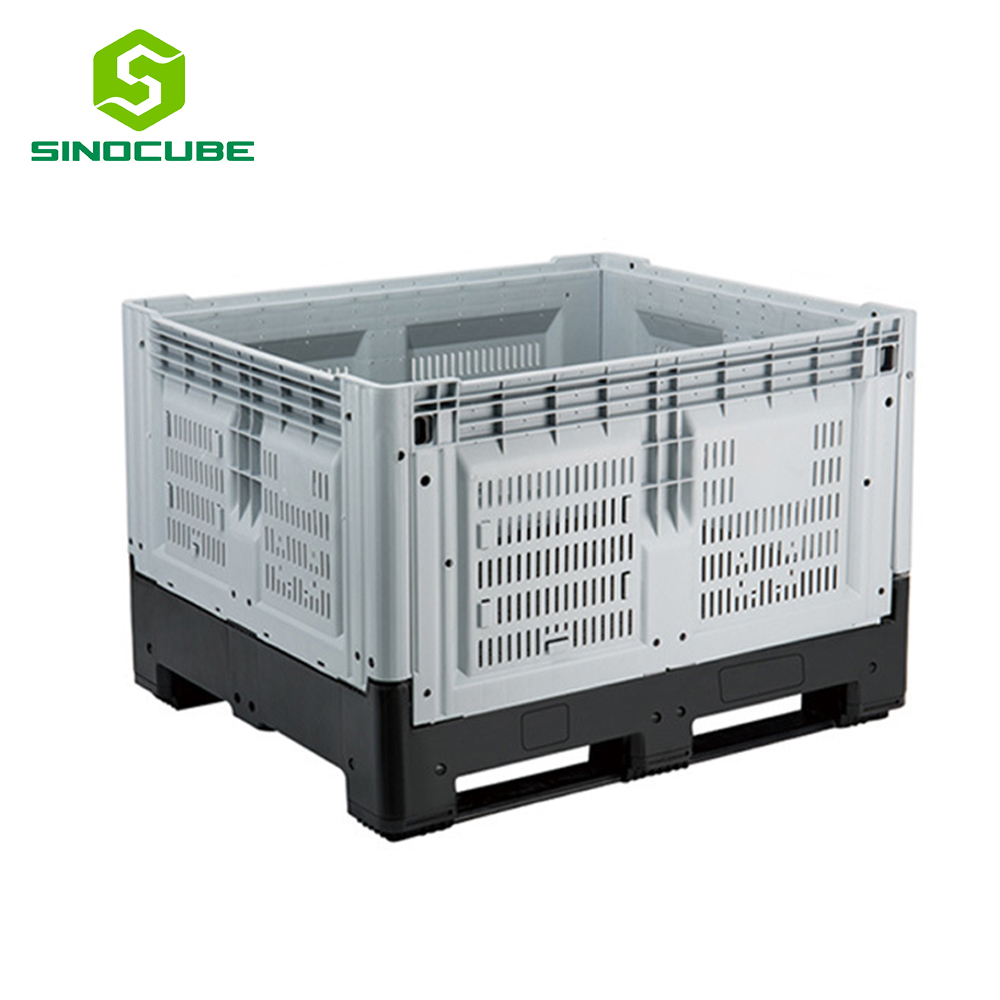
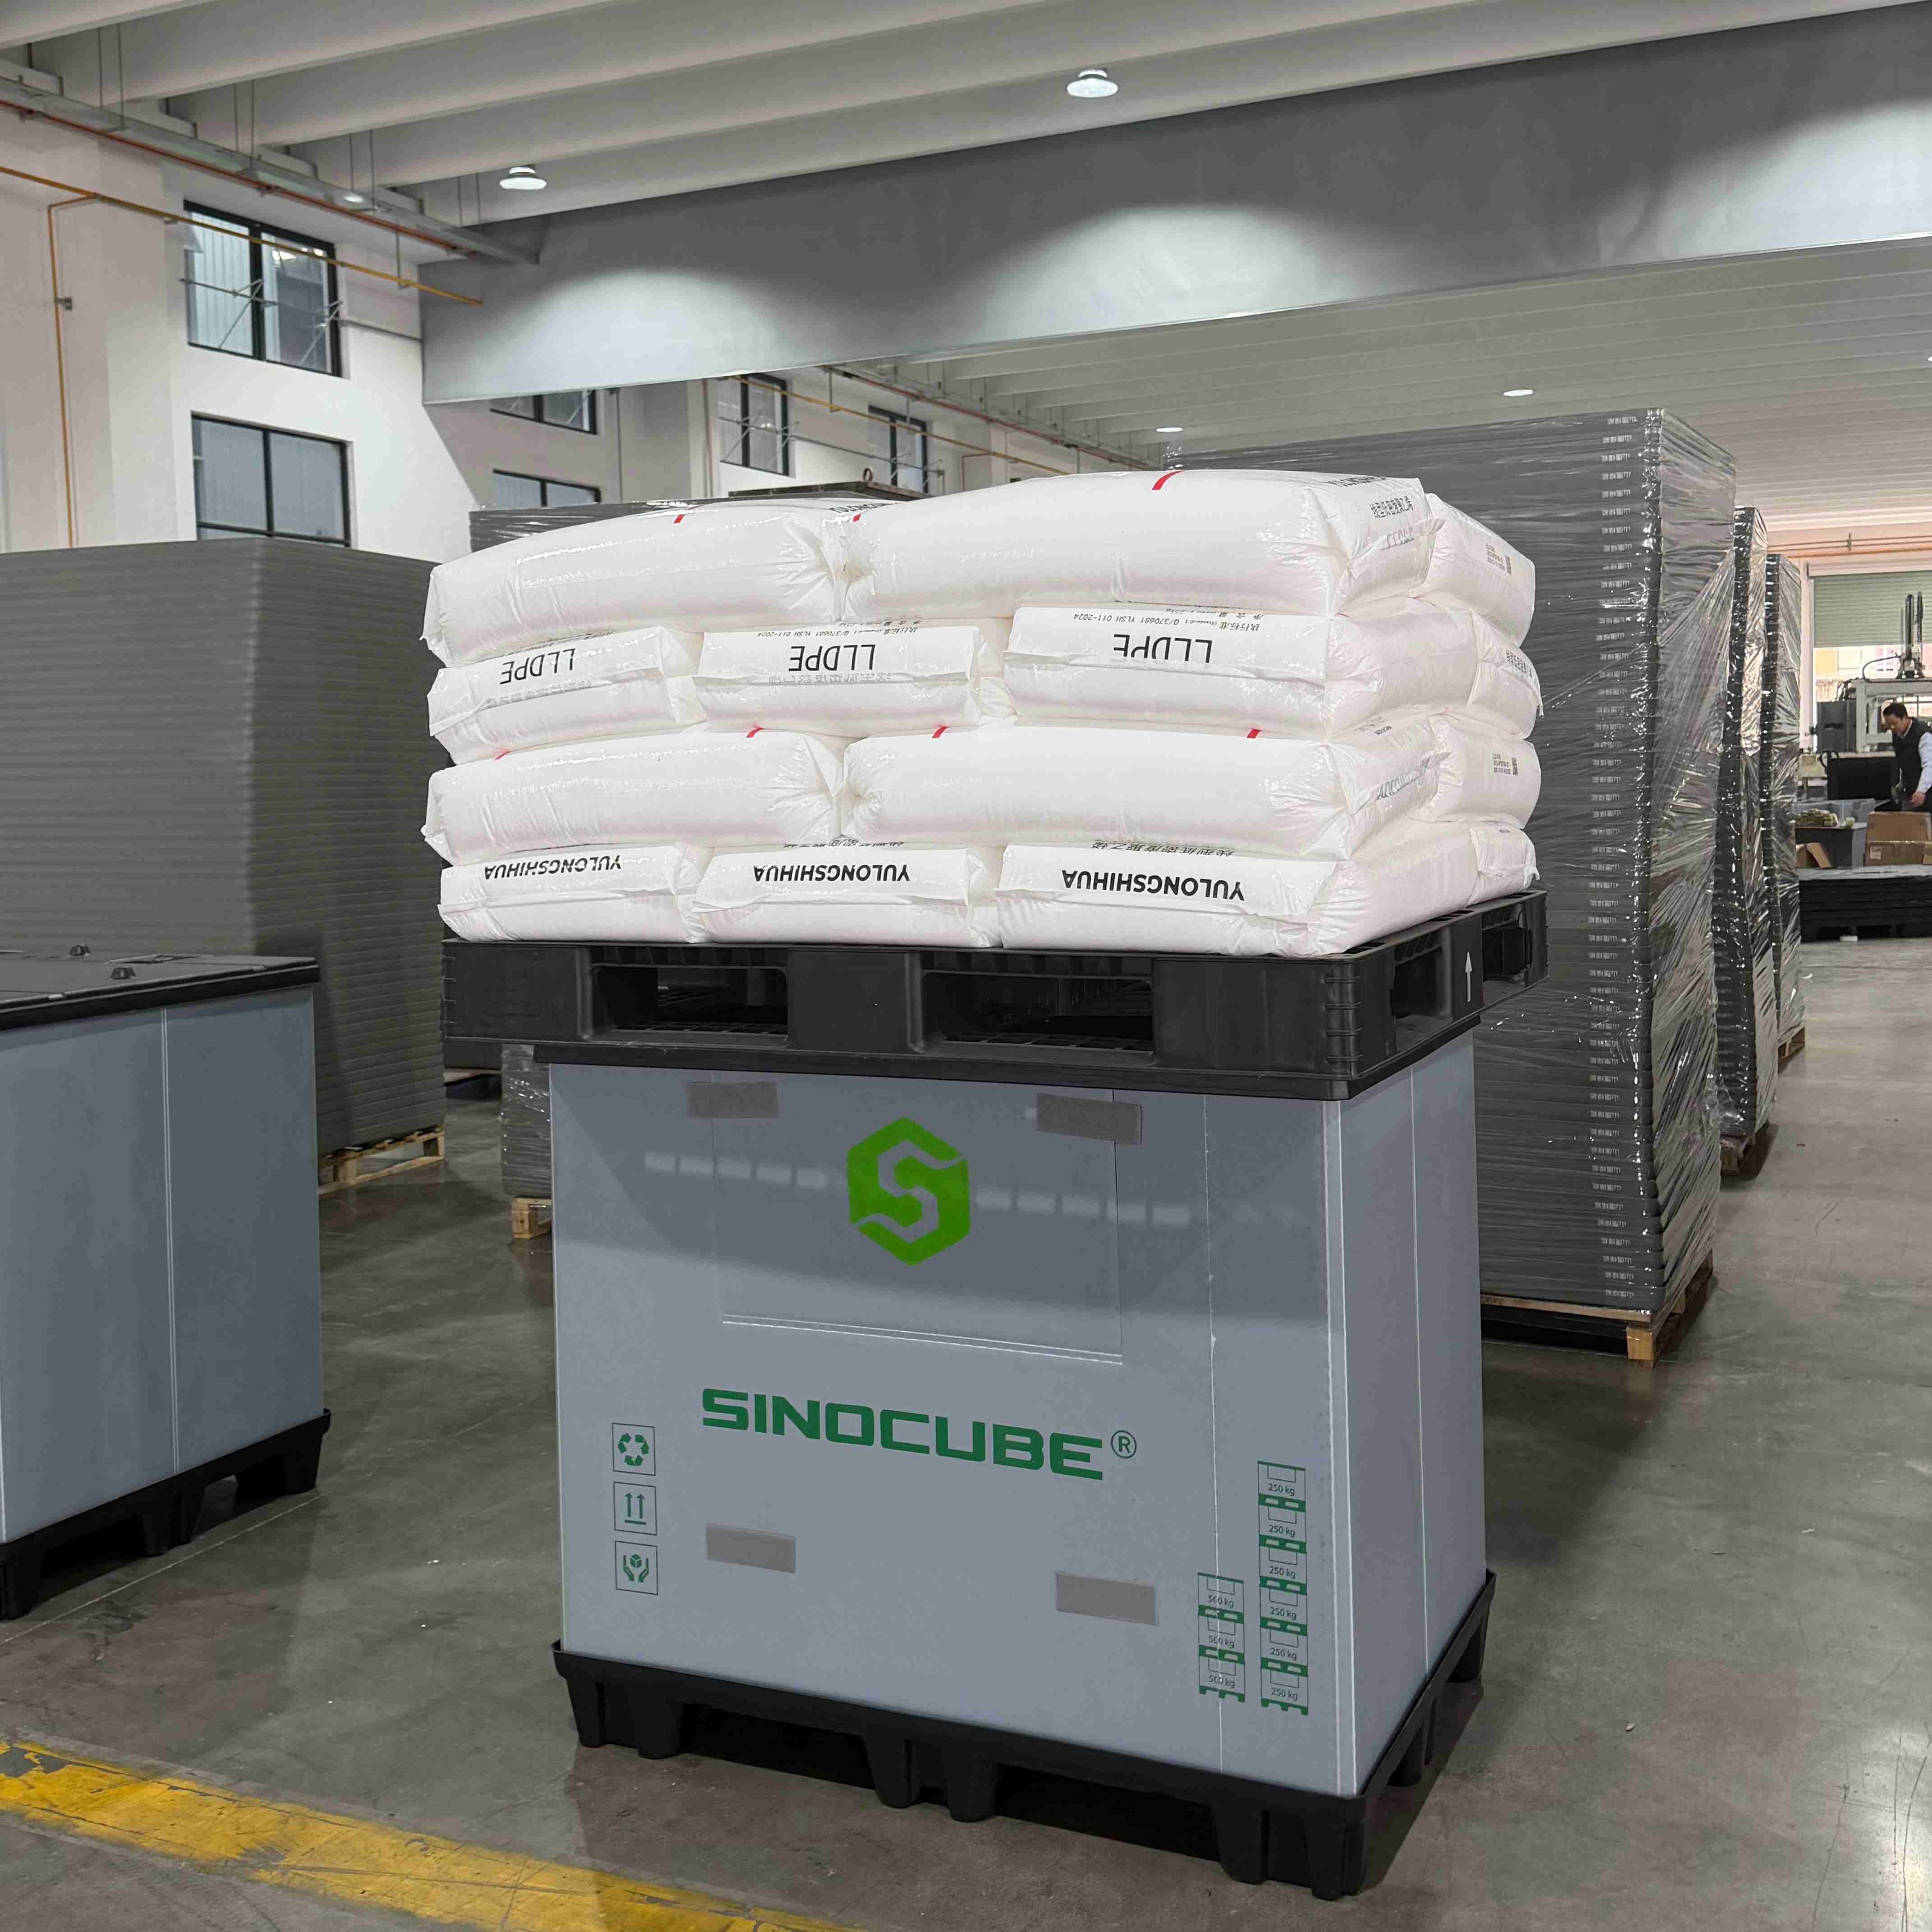
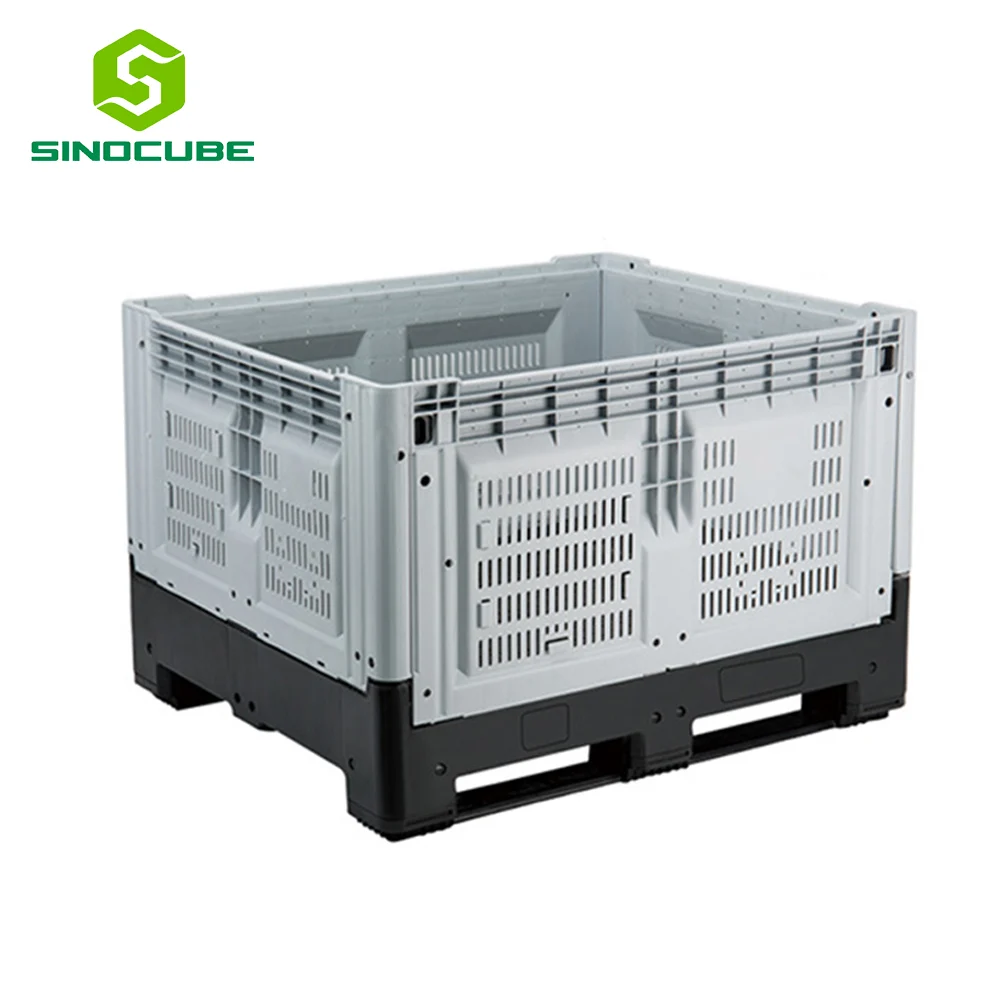
Bulk pallets are essential industrial platforms designed for the efficient storage, handling, and transportation of large quantities of goods across warehouses, distribution centers, and manufacturing facilities. These heavy-duty pallets serve as the foundation for modern supply chain operations, enabling businesses to consolidate products into manageable units that can be moved using forklifts, pallet jacks, or automated handling systems. Bulk pallets are engineered to support substantial weight loads while maintaining structural integrity throughout repeated use cycles. Available in various materials including wood, plastic, and metal, these pallets accommodate diverse industry requirements from food processing to automotive manufacturing. The standardized dimensions of bulk pallets facilitate seamless integration with existing warehouse infrastructure, racking systems, and transportation vehicles. Advanced bulk pallets incorporate features such as reinforced decking, multiple entry points for handling equipment, and stackability to maximize vertical storage space. These platforms play a critical role in reducing manual handling, improving workplace safety, and accelerating loading and unloading operations. The robust construction of bulk pallets ensures they withstand harsh environmental conditions, repeated impacts, and continuous use in demanding operational environments. Modern bulk pallets often include identification systems such as RFID tags or barcodes to enable inventory tracking and supply chain visibility, making them indispensable tools for businesses seeking to optimize logistics efficiency and reduce operational costs.
New Product Recommendations

Investing in quality bulk pallets delivers immediate operational improvements and long-term cost savings for businesses handling large volumes of products. These platforms dramatically reduce labor requirements by enabling workers to move hundreds of items simultaneously rather than handling individual pieces, directly lowering payroll expenses and increasing productivity. The standardized footprint of bulk pallets ensures compatibility with existing material handling equipment, eliminating the need for costly infrastructure modifications. Businesses experience faster order fulfillment as bulk pallets streamline loading and unloading processes, reducing vehicle dwell times and improving delivery schedules. The durability of bulk pallets translates to extended service life, minimizing replacement frequency and reducing total cost of ownership compared to single-use packaging solutions. Enhanced product protection is another significant advantage, as bulk pallets elevate goods above floor level, protecting inventory from moisture, pests, and contamination while facilitating air circulation around stored products. Safety improvements are substantial, as bulk pallets minimize manual lifting and carrying, reducing workplace injuries and associated compensation costs. The stackability of bulk pallets maximizes warehouse vertical space utilization, allowing businesses to store more inventory within existing facilities without expensive expansion projects. For companies managing seasonal demand fluctuations, bulk pallets provide flexible storage solutions that scale efficiently. Environmental benefits include reduced packaging waste when compared to disposable alternatives, supporting corporate sustainability initiatives. The compatibility of bulk pallets with automated systems enables businesses to implement advanced warehouse technologies, future-proofing operations against evolving industry demands. Ultimately, bulk pallets represent a strategic investment that enhances operational efficiency, reduces costs, improves safety, and positions businesses for scalable growth across diverse market conditions.

Tips And Tricks

Why Plastic Pallets Outperform Wooden Ones in Logistics & Storage

13

Mar

Why Plastic Pallets Outperform Wooden Ones in Logistics & Storage

View More
PP Pallet Sleeve Box: Playing a Vital Role in Auto Parts Transportation

13

Mar

PP Pallet Sleeve Box: Playing a Vital Role in Auto Parts Transportation

View More
Why Attached Lid Containers Are the Ideal Choice for Storage & Logistics

13

Mar

Why Attached Lid Containers Are the Ideal Choice for Storage & Logistics

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

bulk pallets

Superior Load Capacity and Structural Integrity

Superior Load Capacity and Structural Integrity

Bulk pallets are specifically engineered to handle extreme weight loads that standard pallets cannot accommodate, making them indispensable for industries dealing with heavy or densely packed materials. The reinforced construction features include thicker deck boards, additional support stringers, and fortified corner blocks that distribute weight evenly across the entire platform. This advanced structural design prevents warping, cracking, and failure even under maximum load conditions during storage or transit. Manufacturing processes incorporate quality-controlled materials tested to industry specifications, ensuring consistent performance across entire pallet inventories. The superior load capacity of bulk pallets enables businesses to consolidate more products per unit, reducing the number of trips required for material movement and decreasing fuel consumption in transportation operations. This consolidation capability directly impacts warehouse efficiency by minimizing handling touchpoints and accelerating throughput rates. The structural integrity of bulk pallets maintains stability during stacking operations, allowing safe vertical storage up to multiple levels without compromising safety or product condition. Businesses benefit from reduced product damage rates as the robust platform prevents shifting and collapse incidents common with inferior alternatives, protecting valuable inventory investments throughout the supply chain.
Versatile Material Options for Diverse Applications

Versatile Material Options for Diverse Applications

The availability of bulk pallets in multiple material compositions allows businesses to select the optimal solution matching their specific operational requirements, regulatory compliance needs, and environmental conditions. Wood bulk pallets offer excellent strength-to-cost ratios and remain the preferred choice for many industries, providing natural shock absorption and easy repairability. Plastic bulk pallets deliver superior hygiene standards essential for food, pharmaceutical, and cleanroom applications, featuring non-porous surfaces that resist bacterial growth and simplify sanitation protocols. Metal bulk pallets provide unmatched durability for extreme-duty applications involving high temperatures, corrosive chemicals, or outdoor storage exposure where other materials would deteriorate rapidly. Each material type offers distinct lifecycle advantages: wood pallets are renewable and biodegradable, plastic variants deliver decades of service with minimal maintenance, and metal options withstand the harshest industrial environments. This material versatility ensures bulk pallets can support operations ranging from refrigerated cold storage to heated manufacturing environments, from moisture-rich agricultural settings to dust-sensitive electronics assembly. Businesses can implement material-specific bulk pallets across different departments within the same facility, optimizing performance and compliance for each unique application while maintaining standardized handling procedures and equipment compatibility throughout their operations.
Enhanced Tracking and Inventory Management Integration

Enhanced Tracking and Inventory Management Integration

Modern bulk pallets incorporate advanced identification technologies that transform basic platforms into intelligent assets within sophisticated supply chain management systems. Embedded RFID chips, durable barcode labels, and QR code markings enable automated scanning and real-time location tracking as bulk pallets move through warehouses, production lines, and transportation networks. This digital integration provides unprecedented visibility into inventory locations, movement patterns, and utilization rates, empowering managers with data-driven insights for operational optimization. Businesses can monitor pallet cycle times, identify bottlenecks in material flow, and optimize warehouse layouts based on actual usage patterns rather than assumptions. The tracking capabilities of equipped bulk pallets facilitate accurate inventory counts, reducing discrepancies between physical stock and system records that often plague manual counting methods. Automated alerts notify managers when bulk pallets require maintenance, approach end-of-life conditions, or deviate from expected movement patterns, enabling proactive management rather than reactive problem-solving. Integration with enterprise resource planning systems allows bulk pallets to trigger automatic reordering, production scheduling, and shipping notifications based on inventory movements. This technological enhancement transforms bulk pallets from passive platforms into active participants in lean manufacturing and just-in-time delivery strategies, reducing carrying costs and improving cash flow through optimized inventory levels across the entire supply chain ecosystem.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000