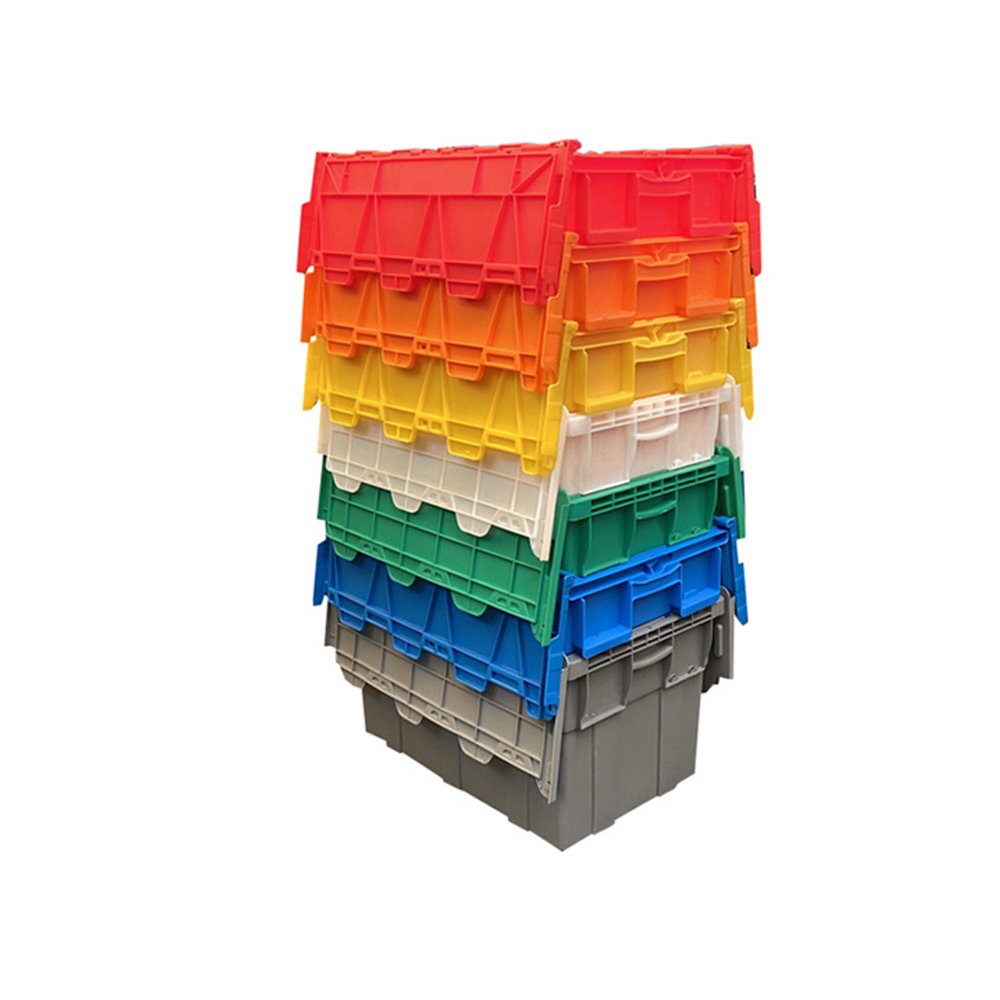
double stacked pallets
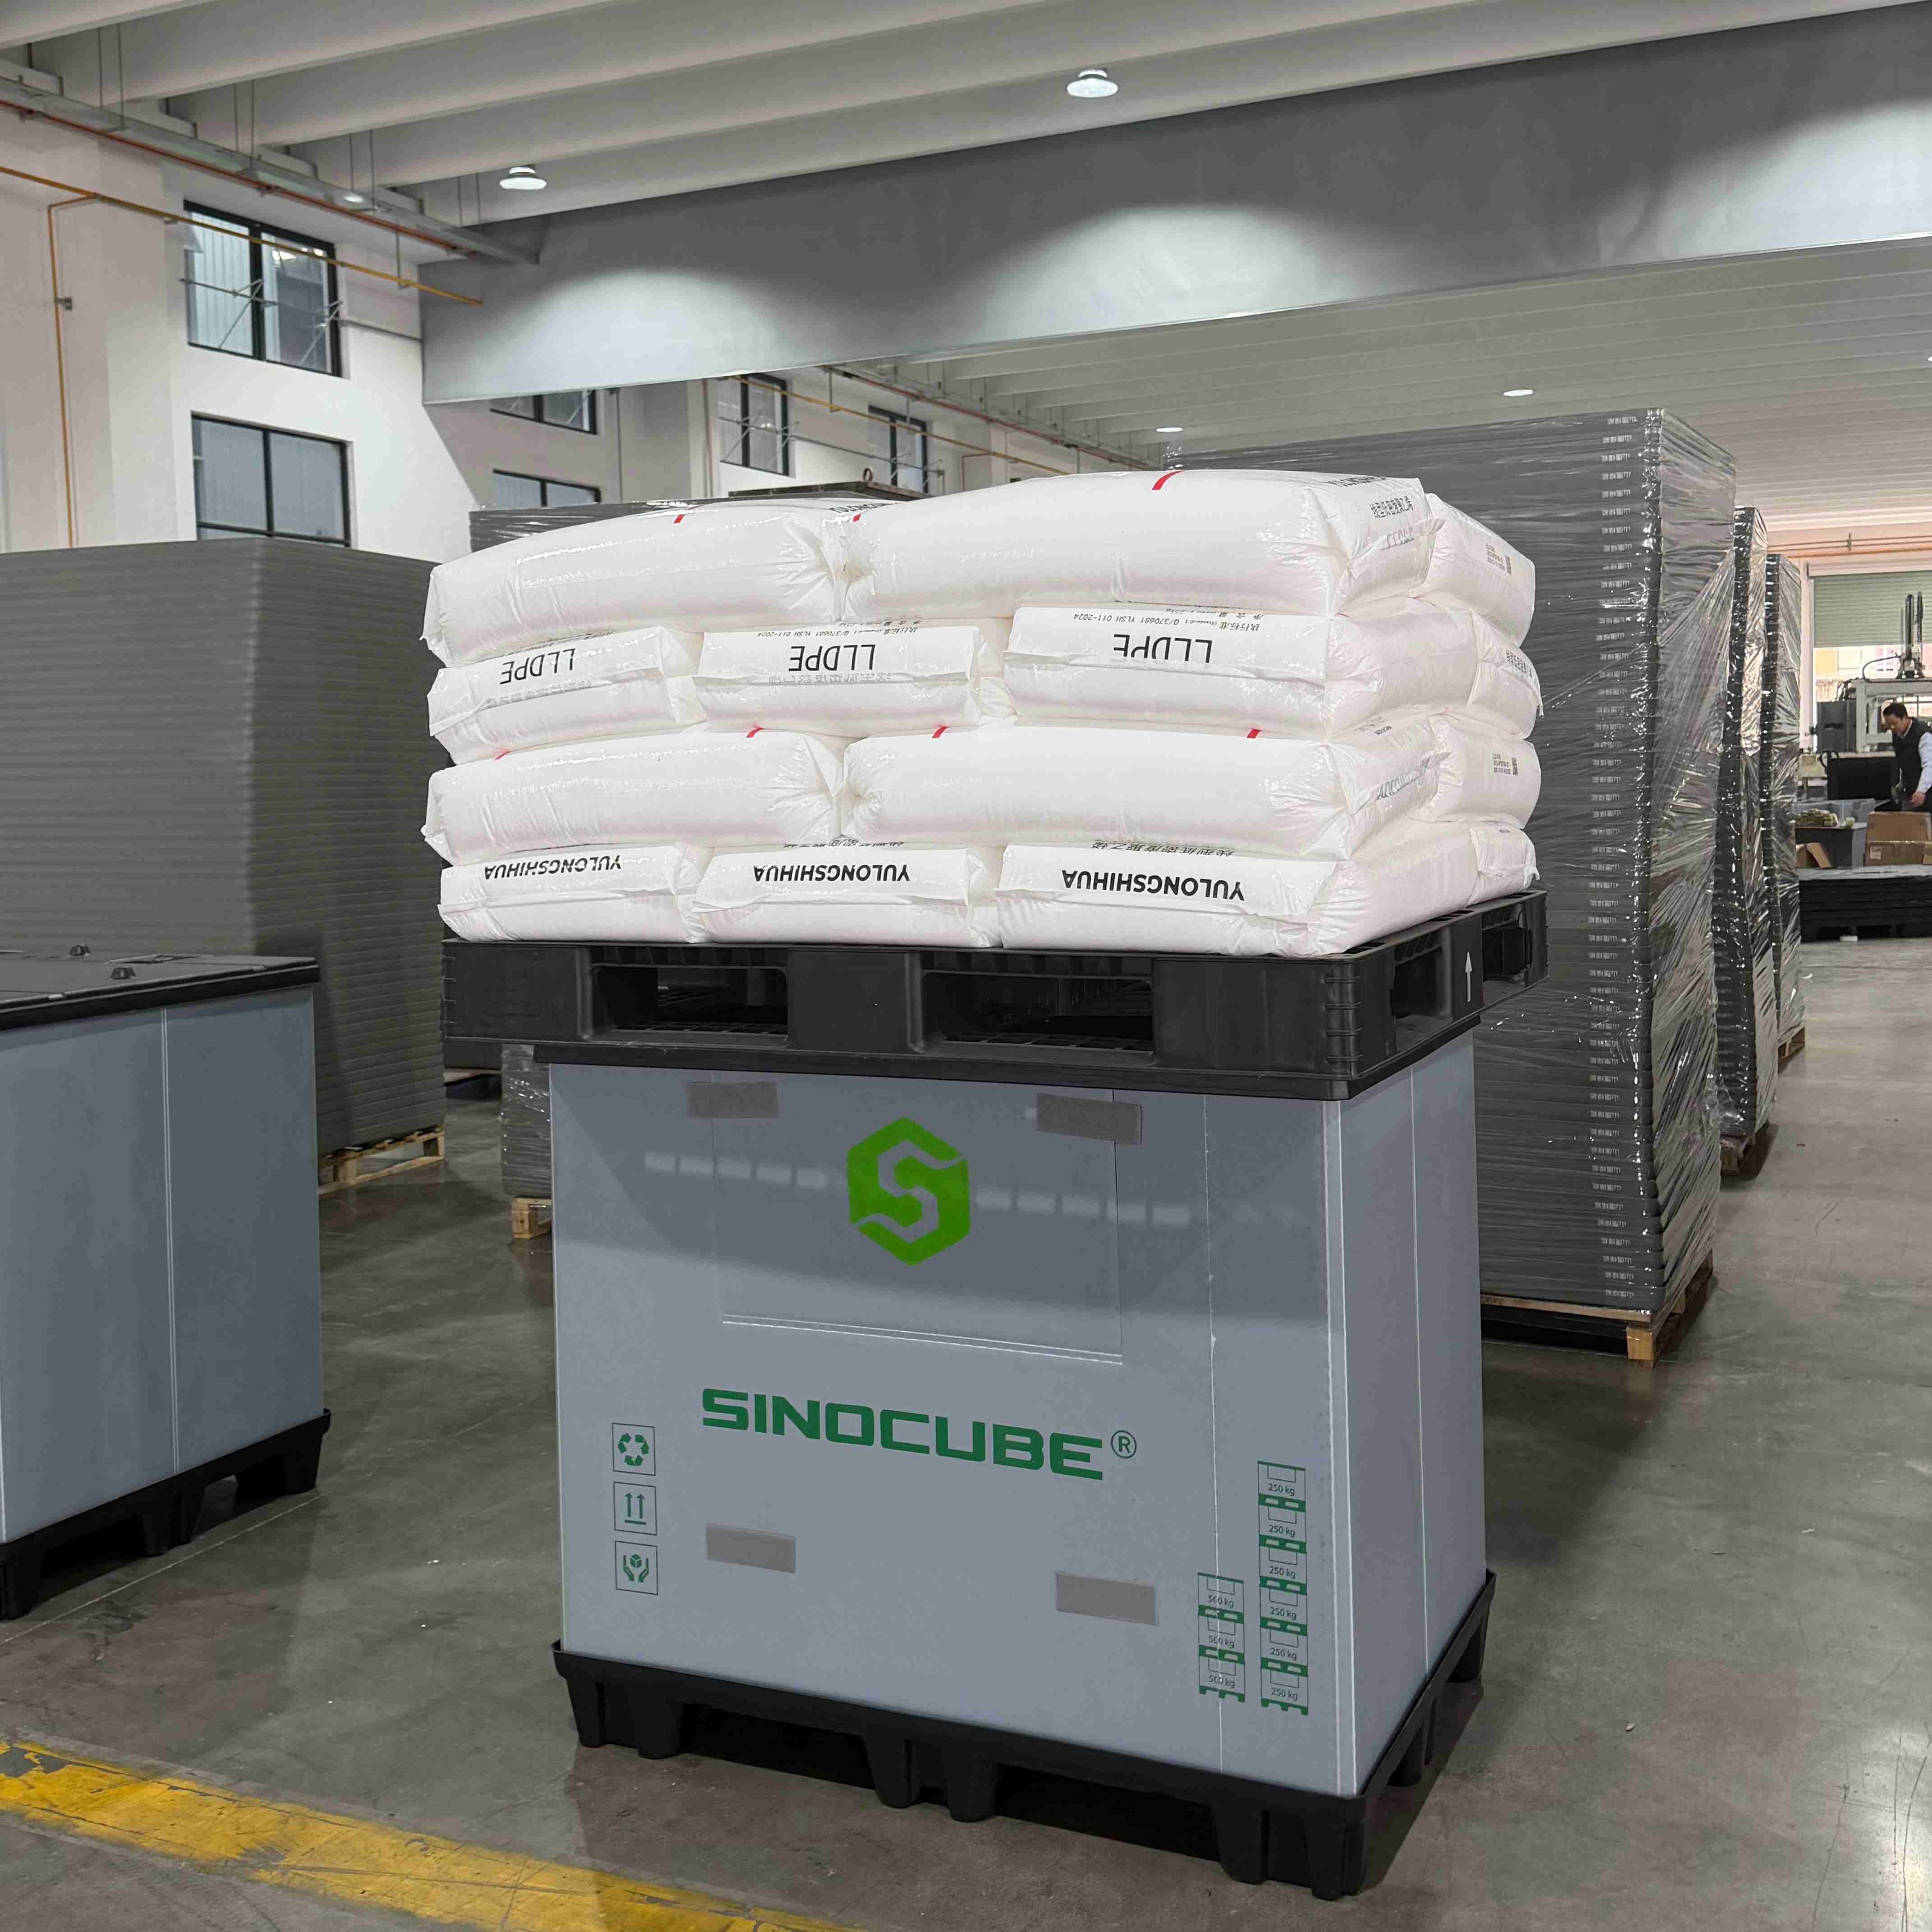
Double stacked pallets represent an innovative warehousing solution that maximizes vertical storage space by safely stacking pallets in two layers. This system utilizes specially designed pallets with reinforced construction and interlocking features that allow one pallet to rest securely on top of another while maintaining load stability. The primary function of double stacked pallets is to optimize storage capacity without requiring additional floor space, making them ideal for facilities with height availability but limited square footage. These pallets incorporate advanced engineering features including reinforced corner posts, enhanced load-bearing capabilities, and precision-molded stacking rims that ensure perfect alignment between layers. The technological design prevents slippage and maintains structural integrity even when fully loaded. Double stacked pallets are manufactured using high-density materials that withstand repeated stacking cycles while protecting goods from damage. Applications span multiple industries including retail distribution centers, manufacturing facilities, cold storage warehouses, and logistics operations. They effectively handle various product types from boxed consumer goods to bulk materials, providing versatility across different operational environments. The system works seamlessly with standard material handling equipment such as forklifts and pallet jacks, requiring no specialized machinery for implementation. By enabling efficient use of cubic space, double stacked pallets help businesses reduce warehousing costs while improving inventory accessibility and organization throughout their supply chain operations.
 EN