Black Pallet Solutions for Modern Logistics

Contact me immediately if you encounter problems!

All Categories

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

black pallet

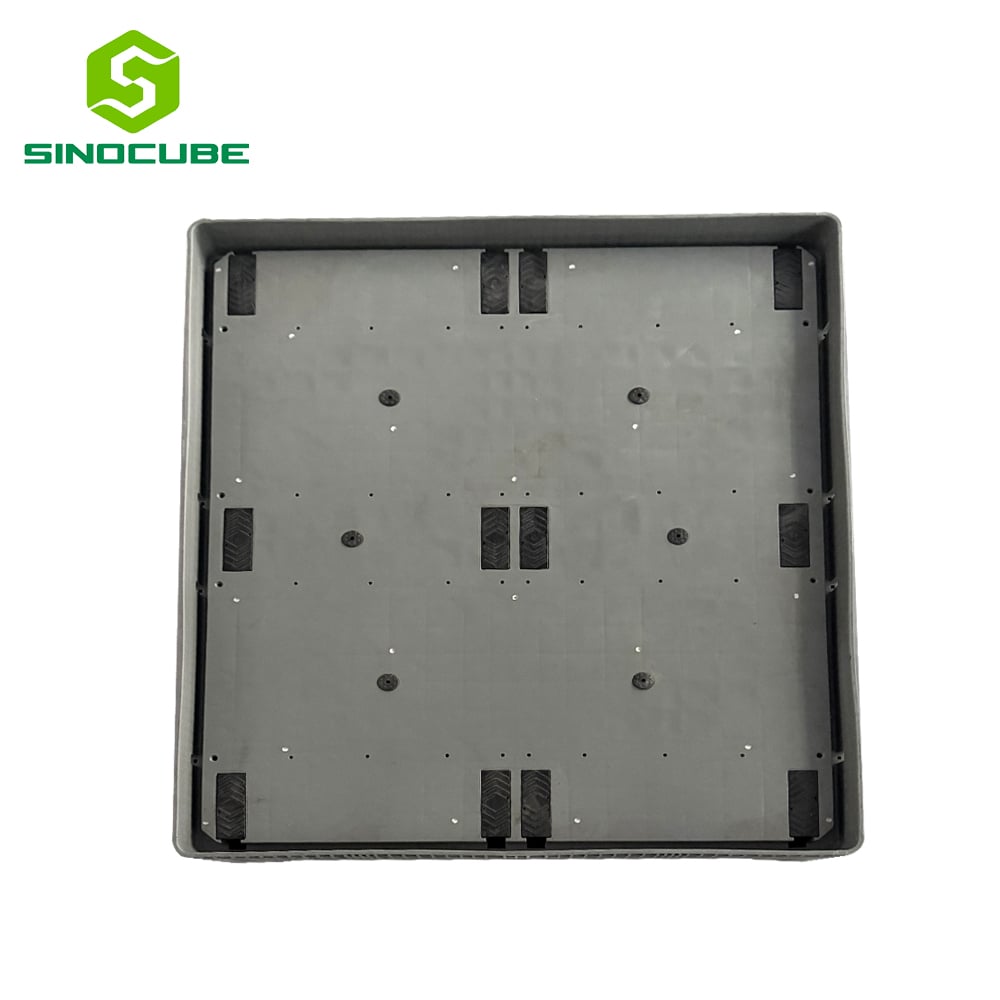
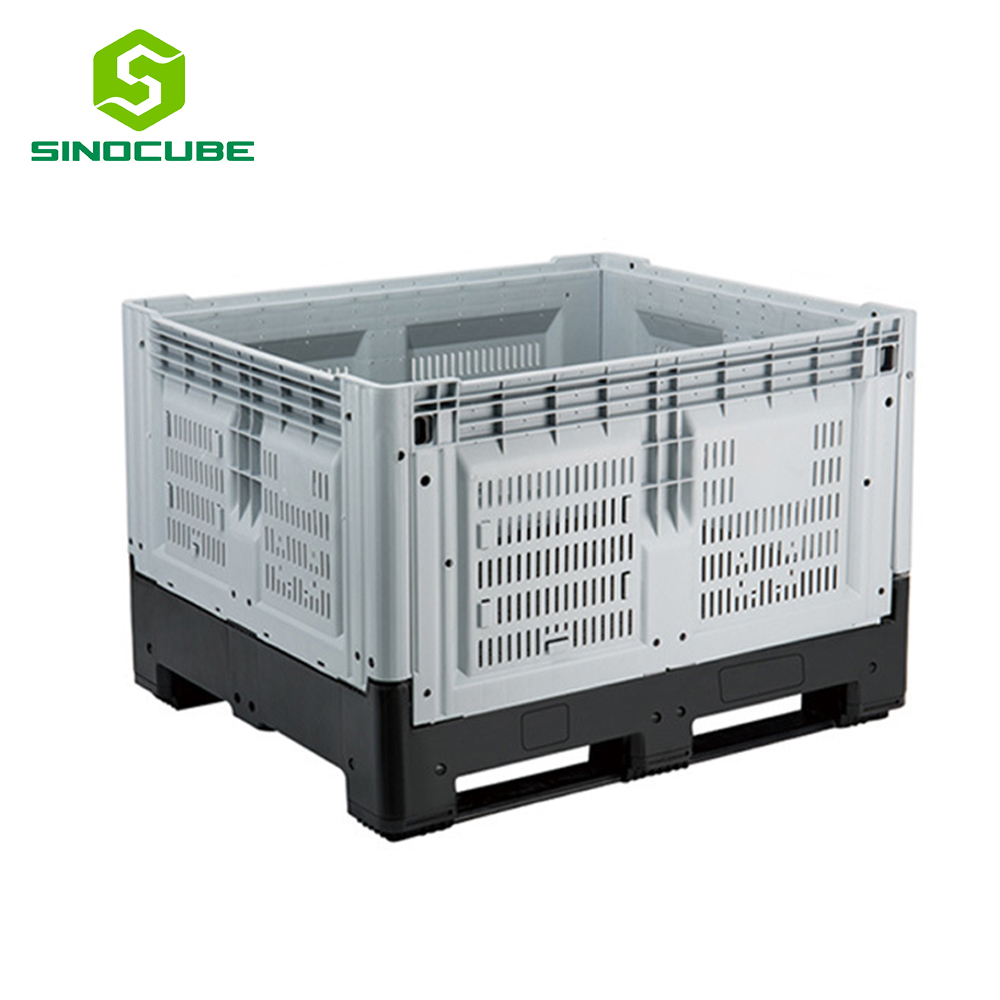
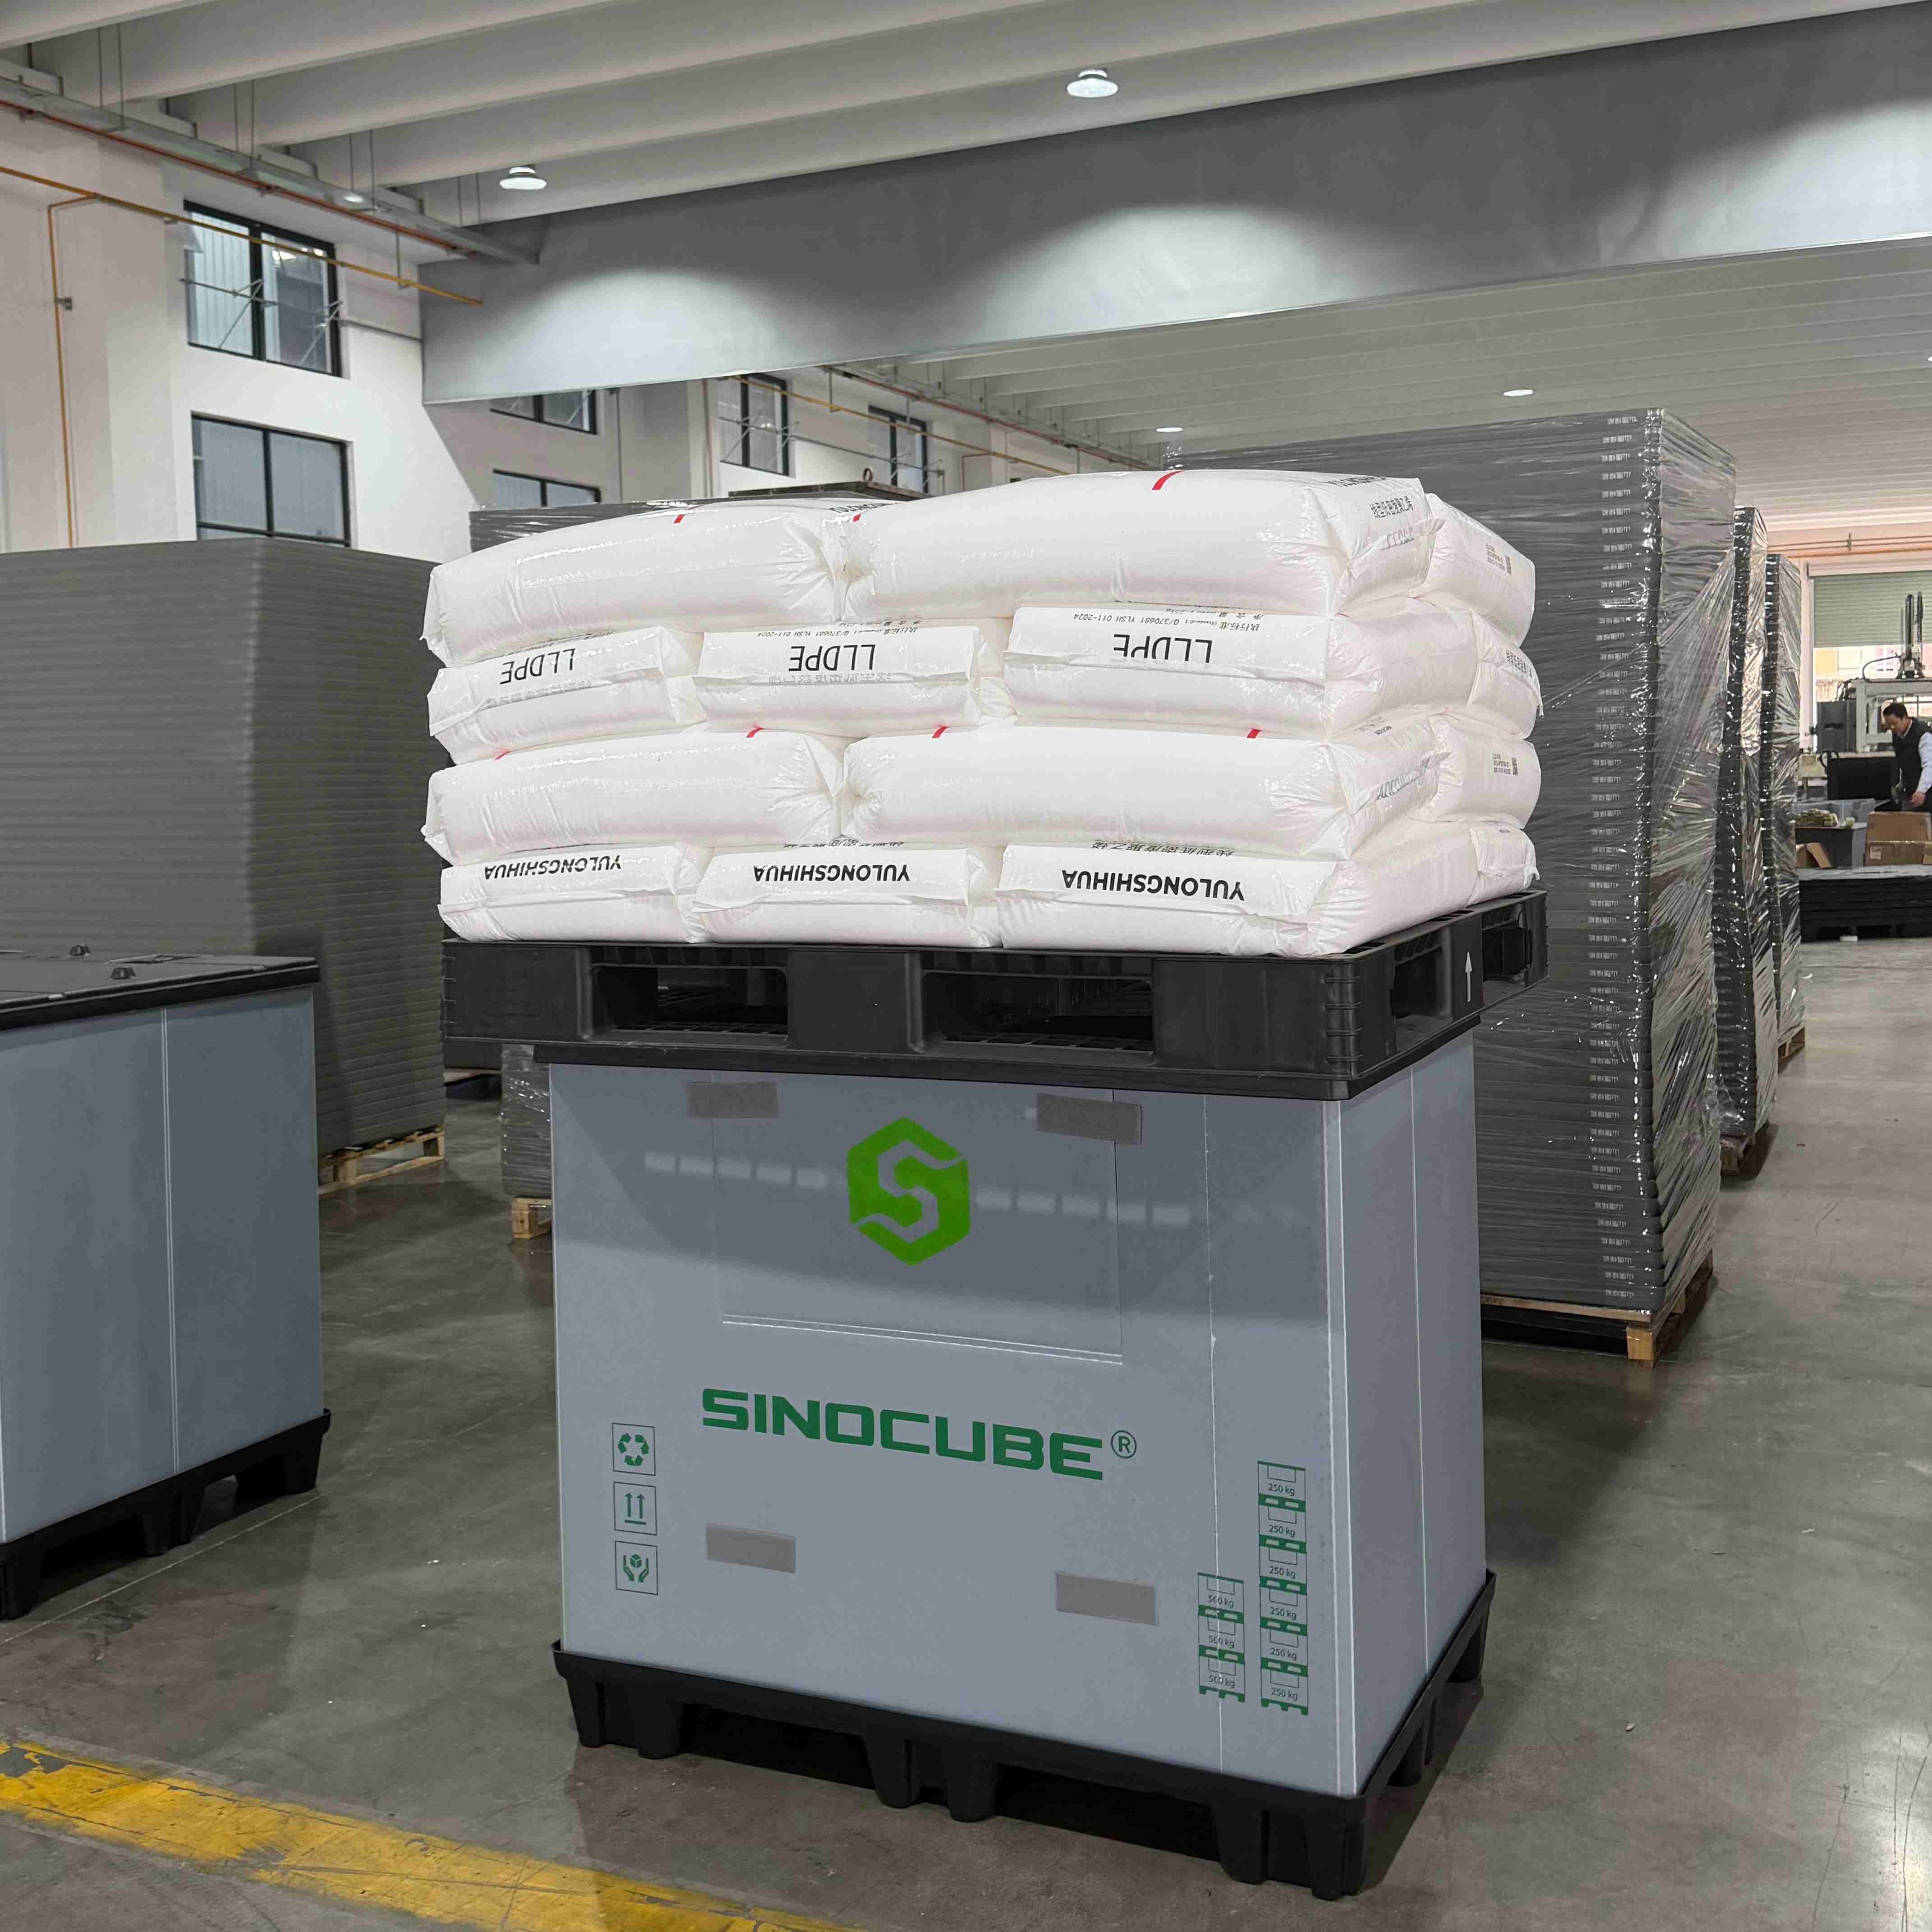
The black pallet represents a modern solution in material handling and logistics operations, designed to meet the demanding requirements of contemporary supply chain management. This specialized platform combines robust construction with a distinctive dark coloration that serves both aesthetic and practical purposes. A black pallet functions primarily as a load-bearing platform that facilitates the efficient movement, storage, and transportation of goods across warehouses, distribution centers, and manufacturing facilities. The dark pigmentation is achieved through advanced manufacturing processes that integrate carbon black or other UV-stabilizing additives directly into the polymer matrix, ensuring color consistency throughout the product's lifespan. Technologically, the black pallet incorporates high-density polyethylene or polypropylene materials that deliver exceptional strength-to-weight ratios, enabling these platforms to support substantial loads while remaining lightweight enough for manual handling when necessary. The manufacturing process employs injection molding or compression molding techniques that create seamless, one-piece construction without weak joints or connection points. These platforms feature standardized dimensions compatible with international shipping containers, automated handling equipment, and racking systems. The surface design typically includes anti-slip textures and drainage channels that prevent load shifting and allow for easy cleaning. Applications span multiple industries including automotive manufacturing, food and beverage distribution, pharmaceutical logistics, retail operations, and export-oriented businesses that require durable, reusable platforms for global shipping networks.
New Product Releases

Choosing a black pallet for your operations delivers tangible benefits that directly impact your bottom line and operational efficiency. The dark coloration provides superior resistance to visible wear, staining, and discoloration compared to lighter alternatives, meaning your equipment maintains a professional appearance throughout years of intensive use. This visual durability proves especially valuable for retail-facing operations and customer-visible areas where presentation matters. The advanced polymer formulations used in black pallet construction offer enhanced UV protection, preventing degradation from sunlight exposure during outdoor storage or transportation, which extends service life significantly and reduces replacement costs. You gain substantial cost savings through the exceptional durability of these platforms, as they withstand repeated impacts, temperature fluctuations, and chemical exposure without cracking or breaking. The non-porous surface resists moisture absorption and bacterial growth, making cleaning and sanitization remarkably simple while meeting strict hygiene standards required in food processing and pharmaceutical applications. Your teams benefit from consistent weight specifications that simplify load calculations and ensure compliance with transportation regulations. The nestable or stackable designs optimize storage space when pallets are empty, reducing warehouse footprint requirements and associated real estate costs. Compatibility with automated handling systems, including conveyor belts, robotic picking stations, and automated guided vehicles, enables seamless integration into modern warehouse management systems. The recyclable nature of polymer construction supports your sustainability initiatives while the extended lifespan means fewer replacements enter the waste stream. Investment in a black pallet proves economically sound through multi-year service capabilities that dramatically lower your per-use cost compared to disposable alternatives, while the consistent quality eliminates product damage risks associated with deteriorating wooden platforms.

Practical Tips

Why Plastic Pallets Outperform Wooden Ones in Logistics & Storage

13

Mar

Why Plastic Pallets Outperform Wooden Ones in Logistics & Storage

View More
PP Pallet Sleeve Box: Playing a Vital Role in Auto Parts Transportation

13

Mar

PP Pallet Sleeve Box: Playing a Vital Role in Auto Parts Transportation

View More
Why Attached Lid Containers Are the Ideal Choice for Storage & Logistics

13

Mar

Why Attached Lid Containers Are the Ideal Choice for Storage & Logistics

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

black pallet

Superior Weather Resistance and Longevity

Superior Weather Resistance and Longevity

The black pallet excels in outdoor applications and challenging environmental conditions through its engineered resistance to ultraviolet radiation and temperature extremes. The incorporation of carbon black and specialized stabilizers throughout the material composition creates a protective barrier against sun exposure that would rapidly degrade unprotected plastics or cause wooden alternatives to crack and splinter. This weather-resistant formulation enables these platforms to withstand extended periods of outdoor storage without structural compromise, maintaining load-bearing capacity through scorching summers and freezing winters alike. Manufacturing facilities with outdoor loading areas, agricultural operations, and businesses lacking covered storage space particularly benefit from this all-weather reliability. The material composition resists warping, swelling, and dimensional changes across temperature ranges from negative forty to positive one hundred sixty degrees Fahrenheit, ensuring consistent performance regardless of climate conditions. Unlike wood that absorbs moisture and becomes heavy or metal that corrodes, the black pallet maintains stable weight and structural integrity through rain, snow, and humidity exposure. This durability translates directly into predictable multi-year service life that enables accurate long-term budgeting and eliminates unexpected replacement expenses that disrupt operational planning.
Enhanced Hygiene and Maintenance Efficiency

Enhanced Hygiene and Maintenance Efficiency

The non-porous surface characteristics of the black pallet deliver significant advantages for industries with stringent cleanliness requirements and contamination prevention protocols. The smooth, sealed surface prevents liquid penetration, bacterial colonization, and pest infestation that commonly plague wooden alternatives with their porous grain structure and potential for harboring contaminants. Food processing facilities, pharmaceutical manufacturers, and healthcare logistics operations benefit from platforms that can undergo high-pressure washing, chemical sanitization, and steam cleaning without degradation or water absorption. The dark coloration effectively conceals minor staining that occurs during normal use while the material itself resists chemical attack from common cleaning agents, oils, and industrial fluids. Maintenance requirements reduce dramatically as these platforms require no painting, sealing, or treatment applications throughout their service life. The absence of protruding nails, splinters, or sharp edges eliminates product damage risks and worker injury potential associated with damaged wooden units. When routine cleaning is performed, the black pallet dries quickly due to its non-absorbent properties, enabling rapid return to service and minimizing operational downtime. This combination of easy maintenance and superior hygiene makes these platforms ideal for regulated industries where contamination prevention is mandatory and audit compliance is critical to maintaining operating licenses.
Optimized Handling and System Integration

Optimized Handling and System Integration

The precisely controlled manufacturing process used to create each black pallet ensures dimensional consistency and weight uniformity that proves essential for automated material handling systems and standardized logistics operations. Every platform meets exact specifications within tight tolerances, enabling reliable performance with conveyor systems, automated storage and retrieval systems, robotic palletizers, and scanning equipment that depend on predictable positioning. The consistent weight characteristics simplify freight calculations and ensure compliance with transportation weight limits without requiring individual weighing of each loaded unit. Forklift operators appreciate the predictable center of gravity and balanced weight distribution that enhances handling safety and reduces equipment strain. The standardized footprint dimensions align with international shipping container widths, maximizing load efficiency and reducing wasted space during transport. Many black pallet designs incorporate features specifically engineered for automation compatibility, including radio frequency identification tag receptacles, barcode mounting surfaces, and edge profiles optimized for sensor detection. The static dissipative formulations available in certain models prevent electrostatic discharge in electronics manufacturing environments where component damage from static electricity poses significant financial risks. Strategic placement of entry points accommodates two-way and four-way forklift access, while optional perimeter lips prevent load overhang and improve stacking stability during storage.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000