 EN
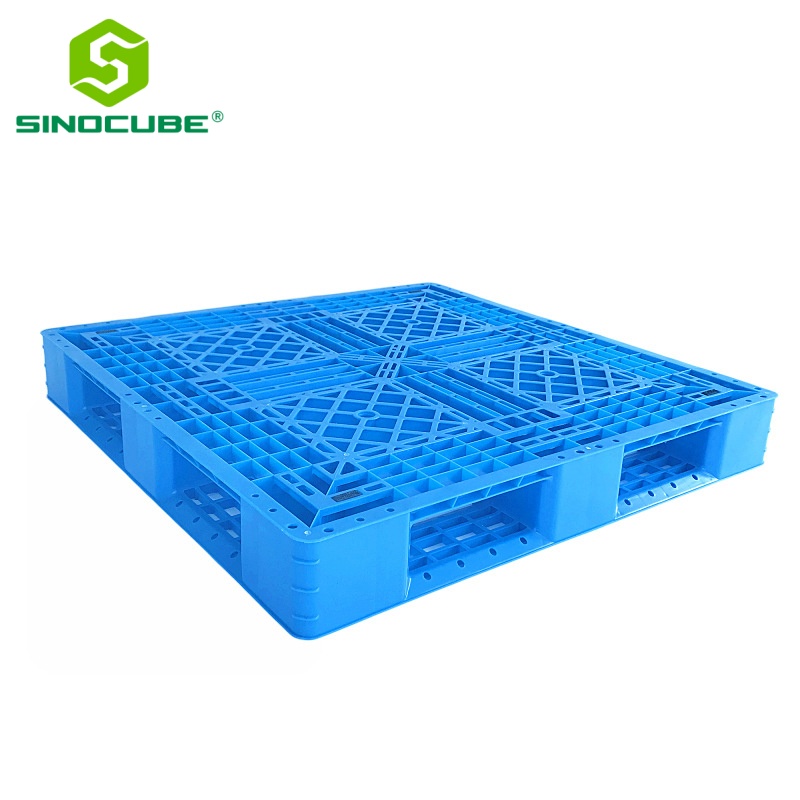
Pallets have become indispensable across numerous industrial sectors, serving as the backbone of modern supply chain management. These standardized platforms enable businesses to transport goods safely while maintaining cost efficiency and operational consistency. Understanding which industries rely most heavily on pallets helps organizations optimize their logistics strategies and improve warehouse productivity.

The widespread adoption of pallets stems from their ability to standardize handling procedures, reduce damage during transit, and facilitate automated warehouse operations. Organizations across industries recognize that investing in quality pallets directly impacts their bottom line through reduced product loss, faster loading times, and improved inventory management. Pallets have revolutionized how businesses approach transportation logistics and material handling efficiency.
Manufacturing and Production Sectors
Heavy Equipment and Automotive Manufacturing
The automotive and heavy equipment manufacturing industries depend critically on pallets for transporting components and finished products. Manufacturers use specialized pallets to secure engine blocks, transmission systems, and automotive assemblies during production and shipment. These pallets protect expensive components from damage while enabling efficient assembly line operations. Heavy-duty pallets support substantial weight loads required for industrial machinery and vehicle parts, making them essential infrastructure in manufacturing facilities worldwide.
Electronics and Technology Production
Electronics manufacturers rely on pallets to handle sensitive components and finished devices with precision. The technology sector uses pallets designed with anti-static properties and protective surfaces to prevent equipment damage during transit. Pallets facilitate the movement of computer hardware, circuit boards, and consumer electronics through various production stages. The ability to stack standardized pallets improves production flow and reduces the risk of costly product damage in high-value manufacturing environments.
Retail and Consumer Goods Distribution
Supermarkets and Grocery Distribution
Grocery retailers and supermarket chains depend on pallets as their primary handling method for bulk product distribution. Pallets enable efficient movement of beverages, canned goods, frozen products, and fresh merchandise from warehouses to retail locations. Distribution centers use pallets to organize shipments by store destination, streamlining the entire supply chain from manufacturer to consumer shelves. The standardization that pallets provide allows supermarket networks to operate large-scale logistics systems serving thousands of retail outlets simultaneously.
Apparel and Consumer Products
Clothing manufacturers and consumer goods distributors use pallets extensively to transport textiles, fashion items, and household products. Pallets accommodate the volume and weight characteristics of packaged consumer goods moving through retail supply chains. These industries benefit from pallets that enable rapid warehouse operations, quick unloading at retail destinations, and efficient inventory rotation. The standardized pallet format helps retailers manage high-velocity product movement and maintain competitive distribution timelines.
Chemical, Pharmaceutical, and Food Processing Industries
Chemical Manufacturing and Distribution
The chemical industry depends on specialized pallets engineered to handle hazardous materials safely during transportation and storage. Pallets used in chemical distribution must meet regulatory compliance standards while protecting workers and the environment from spills and contamination. Pharmaceutical manufacturers require pallets that maintain controlled temperature and humidity conditions for sensitive compounds. These regulated industries recognize that appropriate pallets are not optional but mandatory infrastructure for maintaining safety protocols and regulatory compliance throughout their supply chains.
Food Processing and Cold Chain Logistics
Food processing companies and cold chain logistics providers depend heavily on pallets designed for frozen and refrigerated product transport. Pallets in the food industry must withstand moisture, temperature fluctuations, and regular cleaning procedures required for food safety compliance. These sectors use pallets that maintain product integrity during long-distance distribution while meeting hygiene standards established by regulatory agencies. The food and beverage industry's reliance on pallets stems from both operational efficiency needs and critical food safety requirements that demand reliable, standardized handling equipment.
Construction, Lumber, and Raw Materials Industries
Building Materials and Construction Supply Distribution
The construction industry depends on robust pallets capable of supporting heavy building materials like lumber, steel, and concrete products. Construction suppliers use pallets to organize shipments of drywall, roofing materials, and foundation supplies destined for job sites nationwide. Pallets enable contractors and builders to receive materials efficiently and maintain organized material staging areas at construction locations. The durability requirements for construction material pallets reflect the weight and environmental stress these materials place on handling equipment during transportation and storage phases.
Timber and Lumber Operations
Lumber mills and timber processors rely on industrial-grade pallets designed to withstand rough handling and outdoor storage conditions. Pallets used in forestry supply chains transport raw logs, processed lumber, and wood products to mills, warehouses, and end-use customers. The seasonal nature of timber operations requires pallets that maintain integrity through multiple loading cycles and outdoor weather exposure. Lumber distributors recognize that investing in quality pallets reduces product damage and improves transportation economics for bulky forest products moving through regional and national supply chains.
Pharmaceutical and Medical Device Distribution
Specialized Temperature-Controlled Pallets
Pharmaceutical and medical device companies depend on pallets that integrate temperature monitoring and controlled environment capabilities. Pallets designed for medical supply distribution must maintain specific temperature ranges while providing traceability for regulated products. These industries use pallets equipped with tracking technology that documents product movement and environmental conditions throughout the supply chain. The pharmaceutical sector's reliance on specialized pallets reflects regulatory requirements and the critical importance of maintaining product efficacy and safety for healthcare applications.
Hospital and Healthcare Facility Logistics
Healthcare facilities depend on pallets for internal logistics and receiving operations that move medical supplies, pharmaceuticals, and equipment throughout hospital environments. Pallets in medical settings must meet infection control standards and support rapid inventory management for time-sensitive medical products. Hospitals use pallets to organize emergency supplies, surgical equipment, and patient care materials needed for daily operations. The healthcare industry's dependence on pallets extends beyond warehouses into clinical environments where efficient material handling directly impacts patient care delivery and operational effectiveness.
FAQ
Which industries benefit most from using pallets for transportation?
Manufacturing, retail distribution, food processing, pharmaceuticals, and construction industries benefit most from pallets. These sectors depend on pallets to handle high-volume shipments safely and cost-effectively. Automotive manufacturers, grocery chains, chemical companies, and healthcare facilities all rely on standardized pallets to streamline their complex logistics operations and maintain supply chain efficiency.
How do pallets improve safety in industrial transportation?
Pallets improve safety by securing loads during transit, preventing shifts and damage that could injure workers or contaminate products. Specialized pallets with protective features reduce accidents in warehouses and distribution centers. The standardized design of pallets enables proper equipment compatibility, reducing workplace injuries and product loss throughout transportation and storage operations.
What makes pallets cost-effective for different industries?
Pallets reduce transportation costs through standardization, enabling faster loading and automated handling across industries. They protect products from damage, minimizing financial losses and insurance claims. Reusable pallets provide long-term cost savings compared to alternative packaging methods, making them economically superior for companies moving substantial product volumes through their supply chains regularly.