stackable pallets
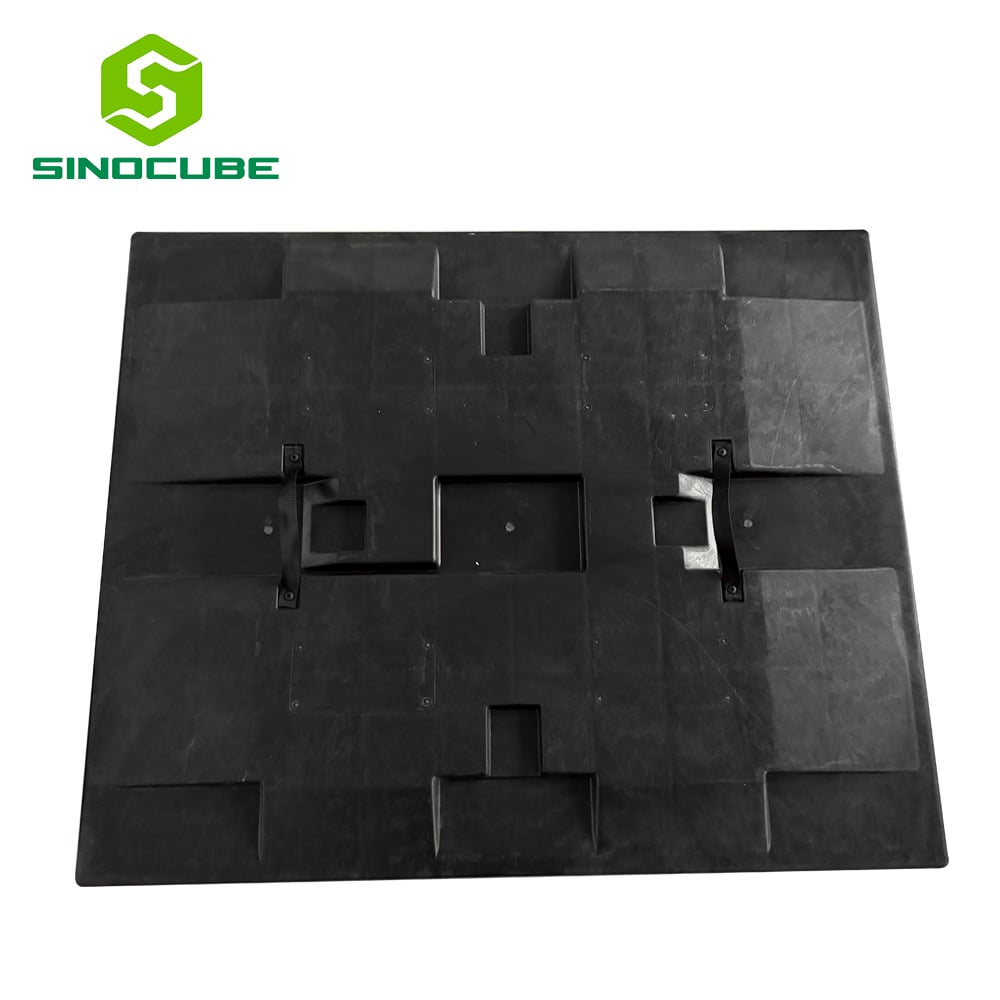
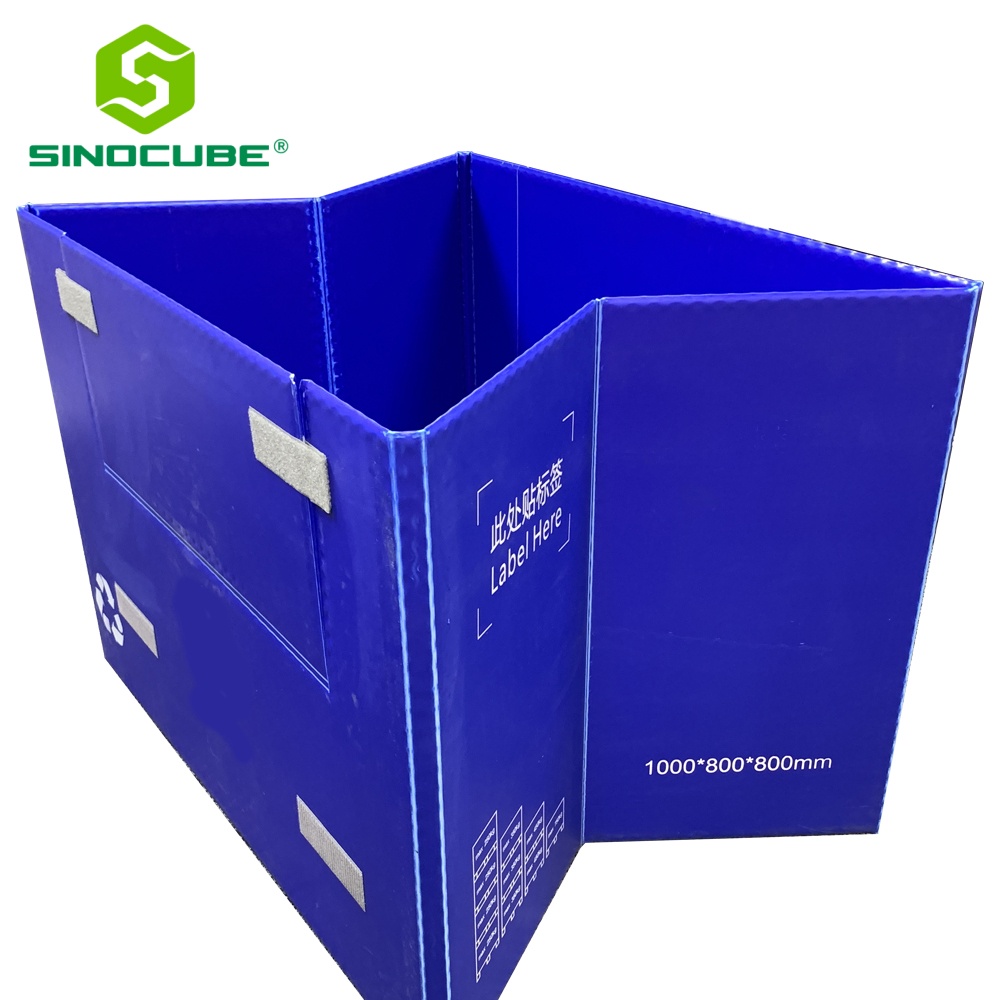
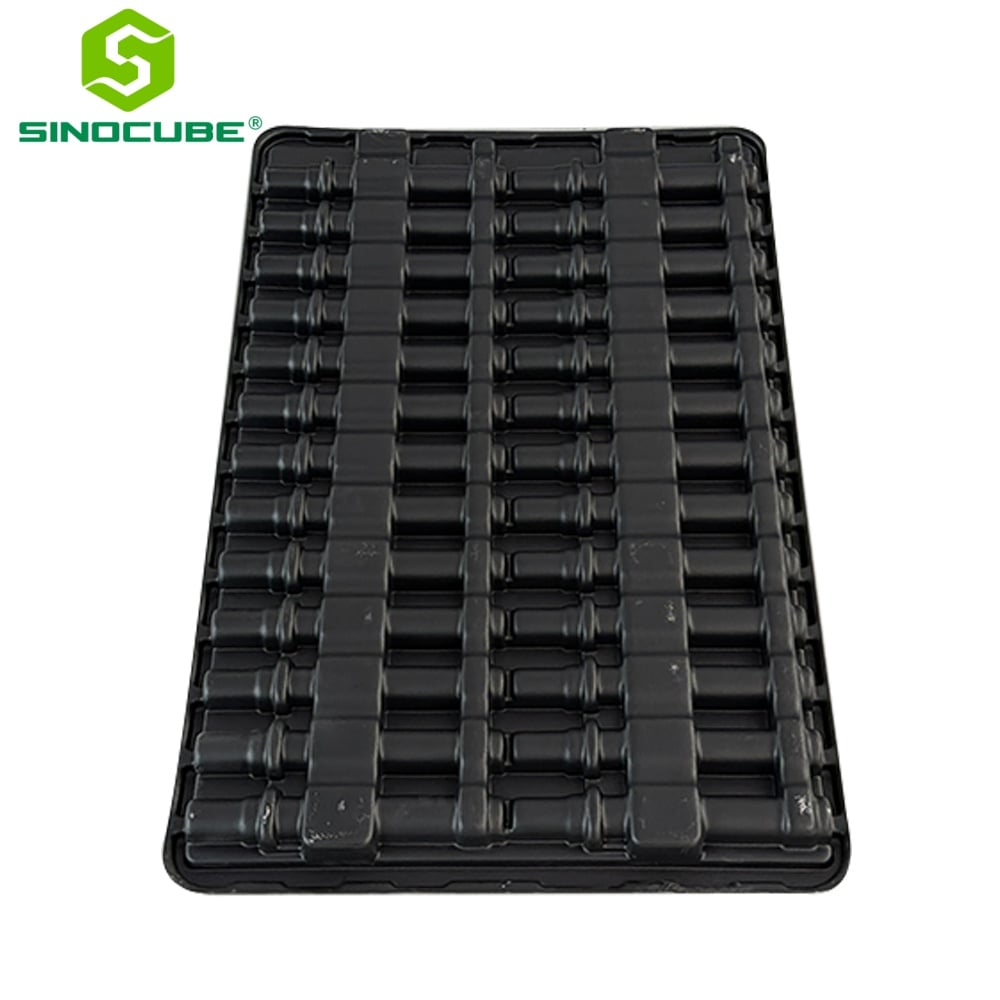
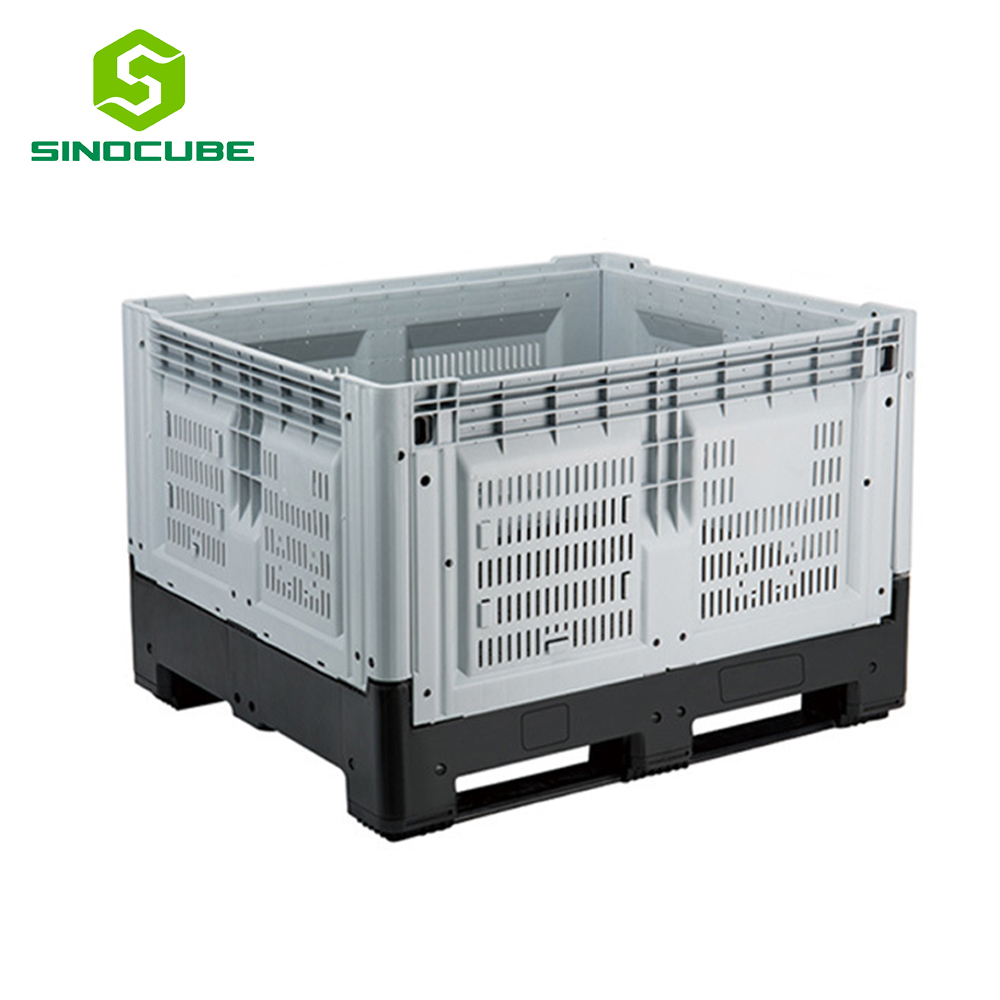
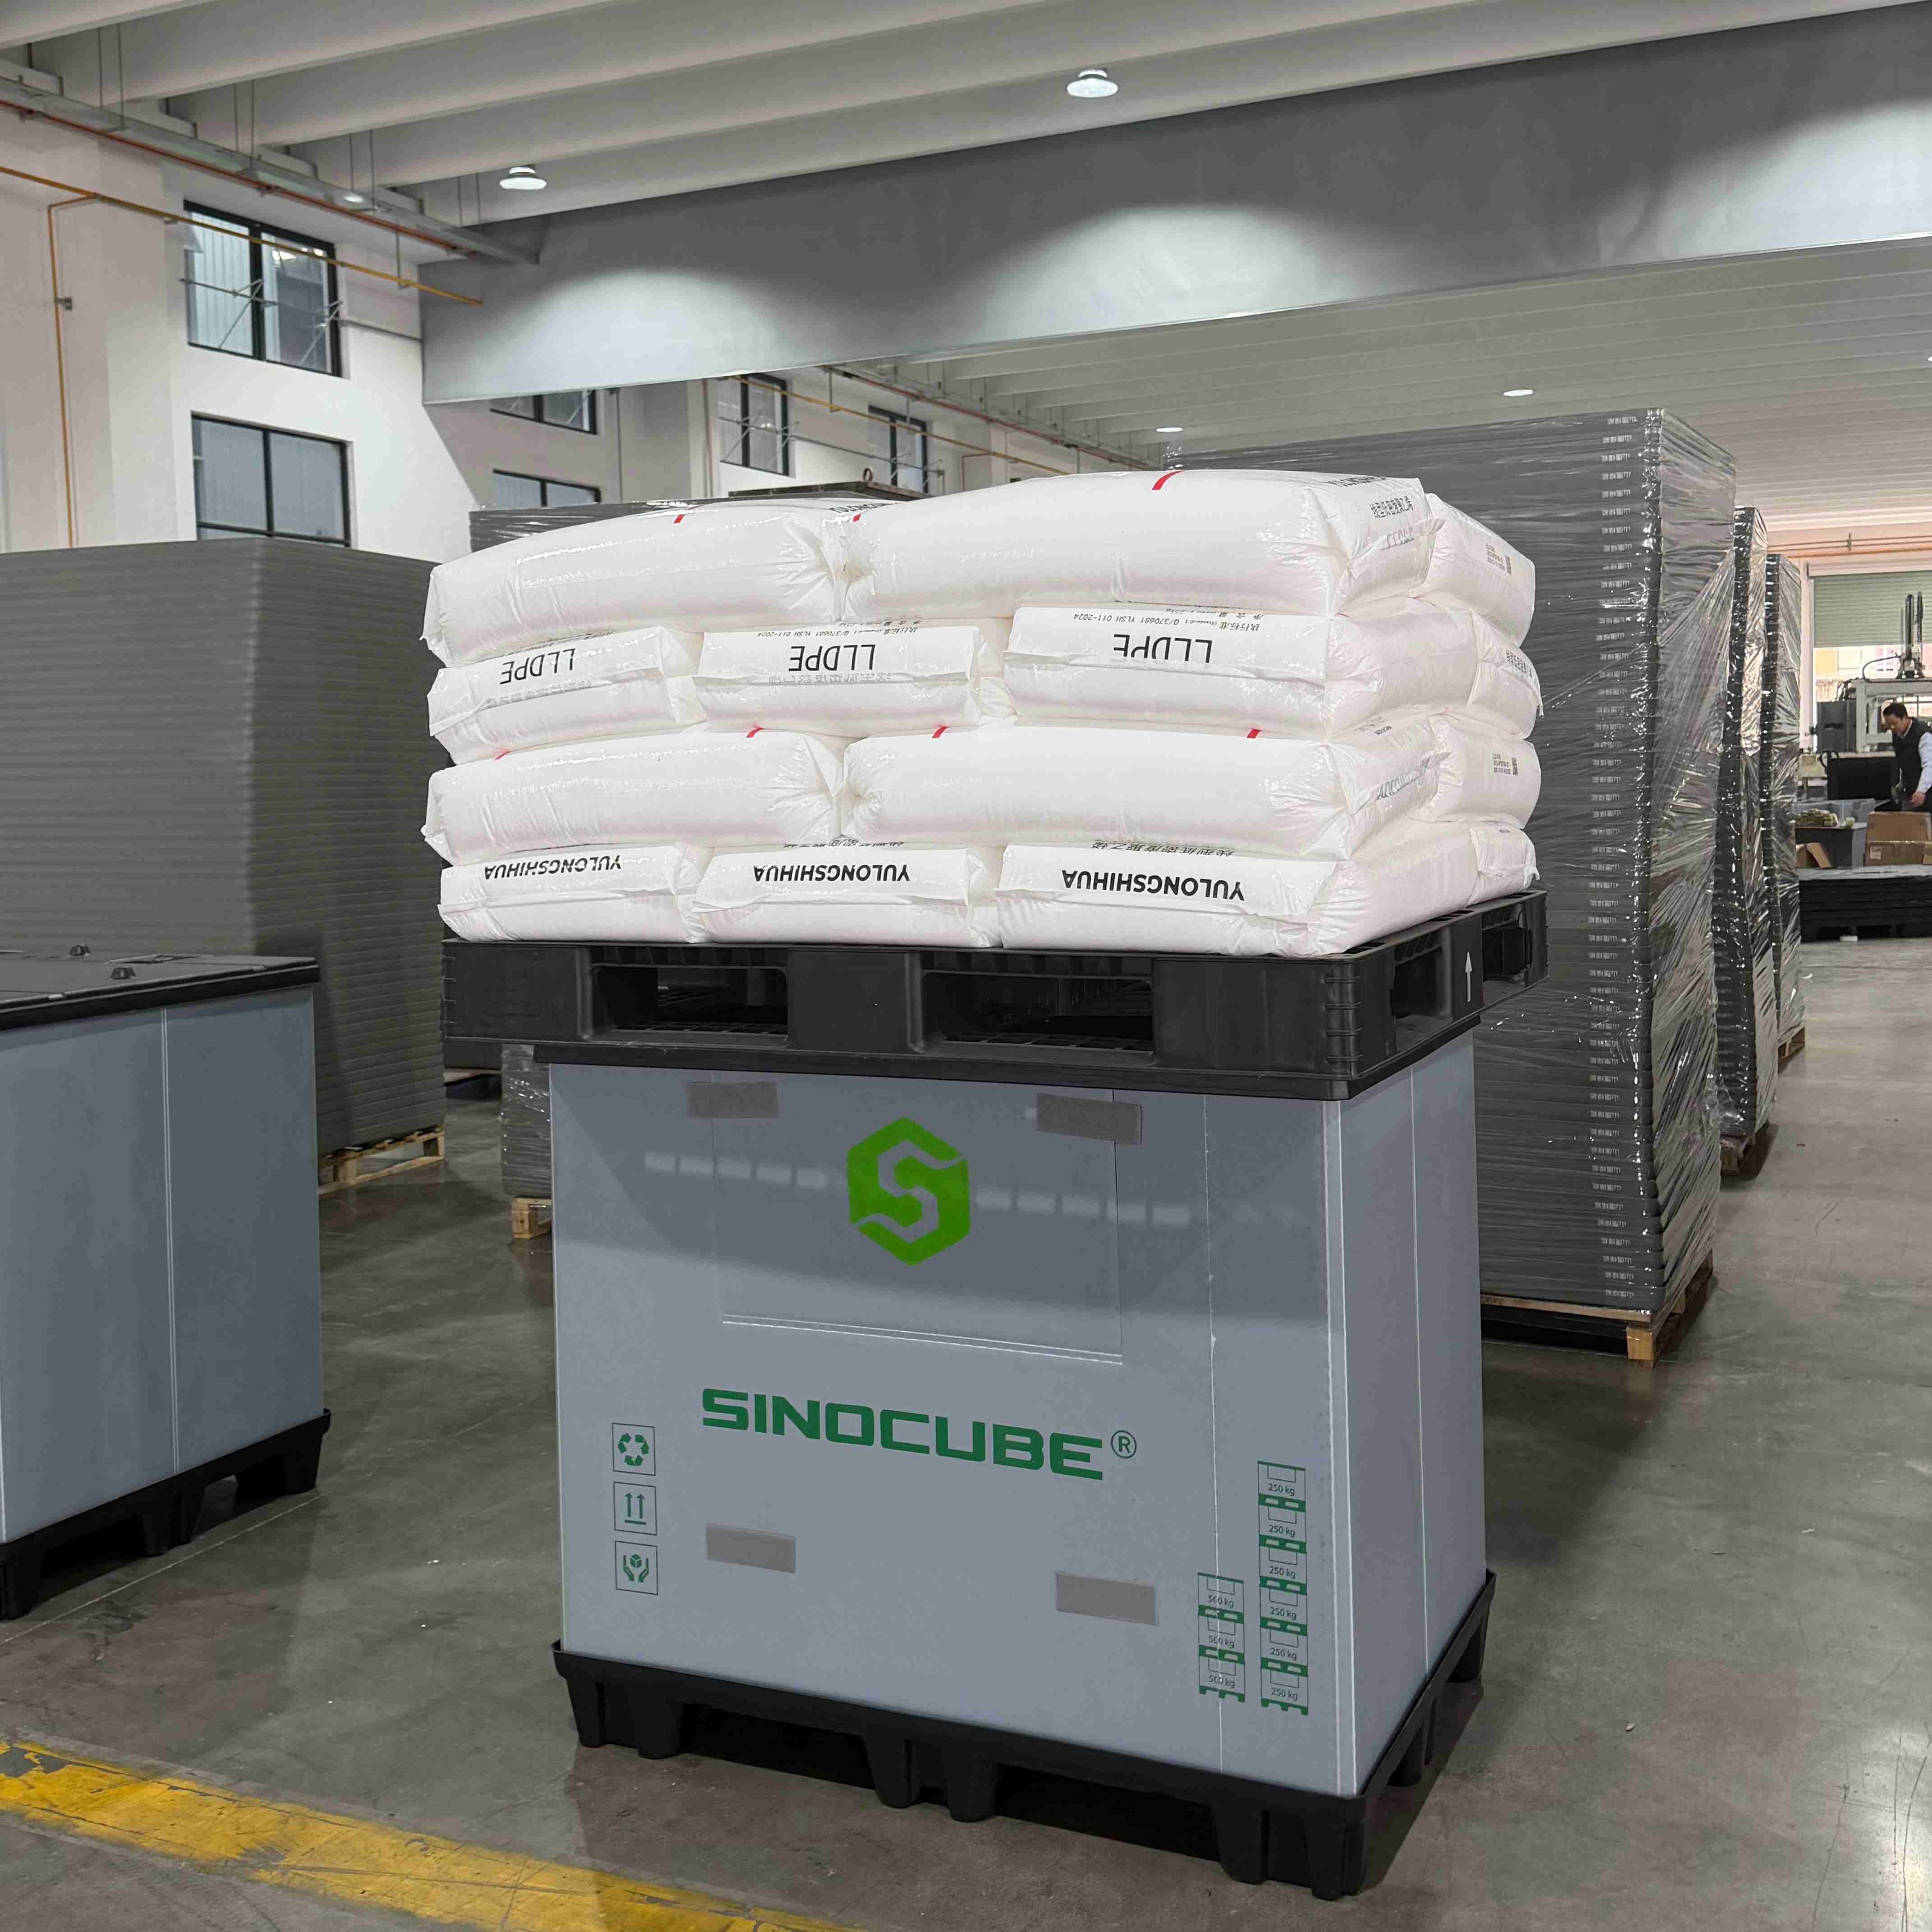
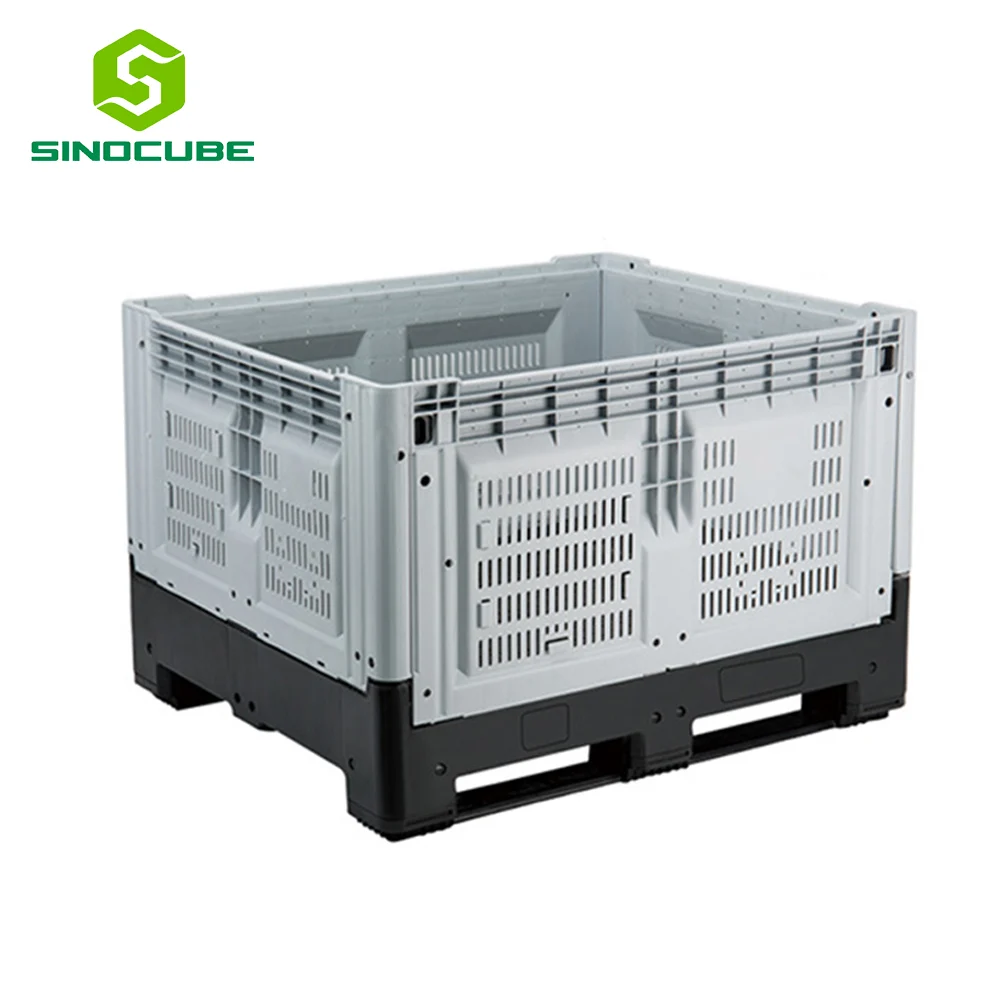
Stackable pallets are essential material handling solutions designed to maximize warehouse storage capacity and streamline logistics operations. These innovative platforms feature a unique structural design that allows them to be safely stacked on top of one another when empty, reducing the floor space required for storage by up to 75 percent compared to traditional pallets. Stackable pallets incorporate reinforced corners, interlocking features, and robust construction that ensures stability during stacking while maintaining excellent load-bearing capacity when in use. The main functions include efficient product transportation, secure goods storage, and optimized space utilization throughout the supply chain. Technological features of stackable pallets encompass precision-molded construction, integrated stacking lips or nesting capabilities, ventilated deck designs for airflow, and durable materials such as high-density polyethylene or polypropylene that resist moisture, chemicals, and temperature variations. These pallets are engineered to comply with international shipping standards and can support both static and dynamic loads ranging from 1000 to 3000 kilograms depending on the model. Applications span diverse industries including food and beverage distribution, pharmaceutical logistics, automotive parts transportation, retail warehousing, and cold storage facilities. Stackable pallets prove particularly valuable in environments where empty pallet storage poses spatial challenges, such as distribution centers with limited square footage, cross-docking operations requiring rapid turnover, and businesses seeking to reduce transportation costs by maximizing the number of empty pallets returned per truckload. Their versatility makes them indispensable for modern supply chain management.
 EN